Stainless Steel Tube Laser Cutting: Nitrogen, Oxygen or Air, Gas Cost per Metre and Oxide-Free Edges
By John Zhao, Service Engineer, PCL Group · Updated 2026-10-29
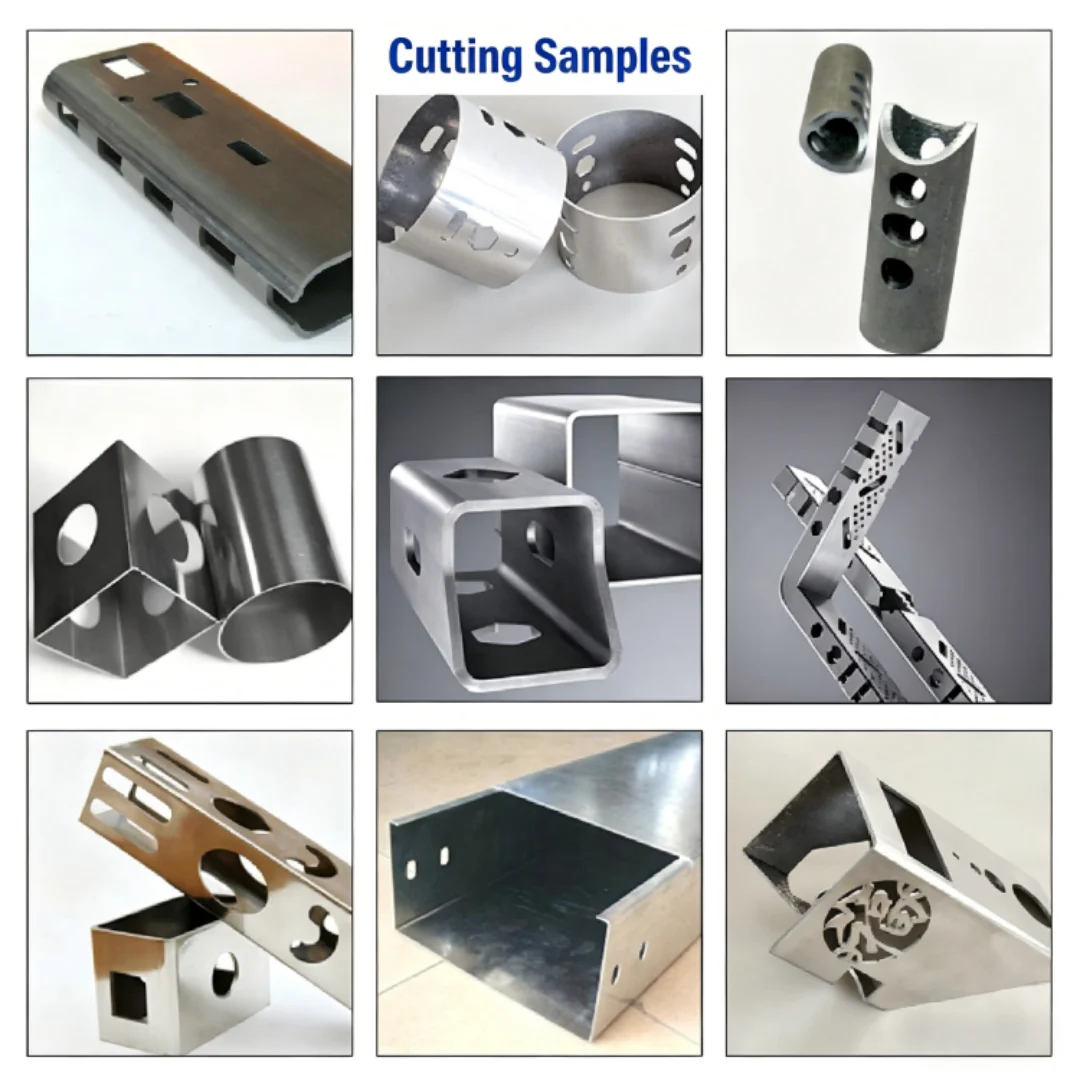
Short answer
- Nitrogen gives a bright, oxide-free edge that welds without grinding; oxygen is faster on thick walls but leaves a dark oxide; air sits in between at the lowest gas cost.
- Nitrogen flow is set by nozzle size and pressure: a 2.0 mm nozzle at 12 bar uses about 23 Nm³ per hour whenever the gas is on.
- Straw or blue edges almost always mean oxygen in the cut: low nitrogen purity, a leak in the gas line or too little pressure.
- Sanitary tube to ASTM A270 or DIN 11850 is thin-wall and fits the LT240; 1.5 kW cuts it, more power buys speed.
On this page
Nitrogen, oxygen or air?
The assist gas decides more about a stainless steel tube than the laser power does. It sets the colour of the edge, whether the part can be welded straight off the machine, and a large share of the running cost. The choice is not the same for every job:
| Nitrogen | Oxygen | Compressed air | |
|---|---|---|---|
| Edge | Bright, silver, oxide-free | Dark oxide layer | Light grey, slight oxide |
| Weld or paint straight away | Yes | Grind or pickle first | Paint yes; visible welds may need cleaning |
| Corrosion resistance at the edge | Kept | Reduced until cleaned | Slightly reduced |
| Pressure | High, about 8-18 bar | Low, below 1-2 bar | High, about 8-16 bar |
| Gas cost | Highest | Low | Lowest: compressor electricity |
| Best for | Food, pharma, furniture, architecture, anything welded or visible | Thick-wall structural stainless where the edge is machined or ground anyway | Thin tube that will be painted or powder coated |
On most stainless tube jobs nitrogen is the answer. Air is worth testing for painted parts under about 3 mm. Oxygen is rarely used on stainless tube because the oxide undoes the reason for buying stainless.
What nitrogen costs per metre
Nitrogen leaves the nozzle at a rate set by the nozzle diameter and the gas pressure, not by the cutting speed. The table gives the approximate flow for a single-hole nozzle, calculated for choked flow with a discharge coefficient of 0.85; measured figures vary a little with nozzle design.
| Nozzle | 8 bar, Nm³/h | 12 bar, Nm³/h | 16 bar, Nm³/h |
|---|---|---|---|
| 1.5 mm | 9 | 13 | 17 |
| 2.0 mm | 16 | 23 | 30 |
| 2.5 mm | 25 | 36 | 47 |
| 3.0 mm | 36 | 52 | 68 |
Cost per metre = flow (Nm³/h) ÷ cutting speed (m/h) × gas price (per Nm³).
A worked example: 1.5 mm stainless tube, 2.0 mm nozzle at 12 bar, 23 Nm³/h, cutting at 10 m/min (600 m/h). Gas used is about 0.039 Nm³ per metre of cut. At a bulk liquid nitrogen price of 0.20 per Nm³ that is under one cent per metre; from cylinders at 1.00 per Nm³ it is about four cents. Prices here are examples in any currency; put in your own supplier’s figure.
Three practical conclusions follow:
- Gas is used whenever the valve is open, including pierces and short moves, so many small holes cost more gas per metre than long contours.
- The smallest nozzle that cuts cleanly saves the most. Going from 2.5 to 2.0 mm cuts flow by over a third at the same pressure.
- Supply matters more than settings. A shop using more than a few cylinders a day usually pays back a liquid tank or an on-site nitrogen generator quickly.
Edge colour: what it tells you
| Edge looks | Likely cause | Fix |
|---|---|---|
| Straw or light gold | Small amount of oxygen: purity below 99.99% or air drawn into the line | Check purity at the machine, tighten fittings, purge the line |
| Blue or purple | More oxygen, or pressure too low to shield the cut | Raise pressure, check regulator and nozzle condition |
| Dark grey or black | Oxygen or air assist, or a burnt nozzle | Switch to nitrogen, change nozzle |
| Silver with fine burr on the underside | Speed slightly high or focus too high | Lower speed in small steps, move focus down into the wall |
| Silver with heavy dross | Speed too low or pressure too low | Increase speed or pressure |
| Spatter inside the tube | Breakthrough energy reaching the far wall | Start cuts on scrap, use micro-joints, check speed |
If edges change colour during a shift with nothing else changed, look at the gas supply first: a cylinder running low, a manifold switching over, or a tank that needs topping up.
Sanitary, food-grade and decorative tube
Hygienic tube for dairy, food, beverage and pharmaceutical plants is made to ASTM A270 in inch sizes or DIN 11850 in metric sizes, usually in 304 or 316L. Parts cut from it are often welded orbitally or by TIG without filler, so the cut end must be square, clean and oxide-free. Nitrogen-cut edges meet that without grinding. Where the specification calls for passivation after fabrication, ASTM A380 and A967 describe the cleaning and passivation methods.
| Standard and size | OD × wall, mm | Machine | Laser and gas |
|---|---|---|---|
| ASTM A270 1″ | 25.4 × 1.65 | LT240 | 1.5 kW, nitrogen |
| ASTM A270 1½″ | 38.1 × 1.65 | LT240 | 1.5 kW, nitrogen |
| ASTM A270 2″ | 50.8 × 1.65 | LT240 | 1.5 kW, nitrogen |
| ASTM A270 3″ | 76.2 × 1.65 | LT240 | 1.5 kW, nitrogen |
| ASTM A270 4″ | 101.6 × 2.11 | LT240 | 1.5 kW, nitrogen |
| DIN 11850 series 2 DN 25 | 29 × 1.5 | LT240 | 1.5 kW, nitrogen |
| DIN 11850 series 2 DN 40 | 41 × 1.5 | LT240 | 1.5 kW, nitrogen |
| DIN 11850 series 2 DN 50 | 53 × 1.5 | LT240 | 1.5 kW, nitrogen |
| DIN 11850 series 2 DN 65 | 70 × 2.0 | LT240 | 1.5 kW, nitrogen |
| DIN 11850 series 2 DN 100 | 104 × 2.0 | LT240 | 1.5 kW, nitrogen |
| DIN 11850 series 2 DN 150 | 154 × 2.0 | LT240 | 1.5 kW, nitrogen |
For polished and brushed decorative tube, keep the protective film on during cutting if it is rated for laser cutting, and handle parts on clean supports so the finish is not scratched by the bed.
Laser power for stainless tube
| Laser power | Maximum stainless, nitrogen | Comfortable production range |
|---|---|---|
| 1.5 kW | 5 mm | Up to about 2-3 mm: furniture, sanitary, railings |
| 3 kW | 8 mm | Up to about 4 mm: equipment frames |
| 6 kW | 14 mm | Up to about 8 mm: thick-wall and process pipe |
| 12 kW | 25 mm | Heavy-wall stainless and maximum speed |
Maximum figures are from the fiber laser cutting speed chart. On thin stainless more power mainly raises speed, which also lowers nitrogen used per metre.
Machines for stainless tube
Most stainless tube work fits the LT240 tube laser with 1.5-3 kW and nitrogen; round chucks are an option for shops that cut mainly round sanitary tube. For long runs of the same tube, the automatic loading tube laser keeps the laser busy between bars. Because stainless costs several times more than carbon steel per metre, the zero-tail LT3 three-chuck series often pays back on material saving alone. Joint fit-up on round tube is covered in round tube laser cutting, and stainless sheet in the stainless steel laser cutter.
Have a cutting job in mind? Send the section size, wall thickness and a drawing, and an engineer will tell you which method or machine fits.
Ask on WhatsAppMachines mentioned in this article
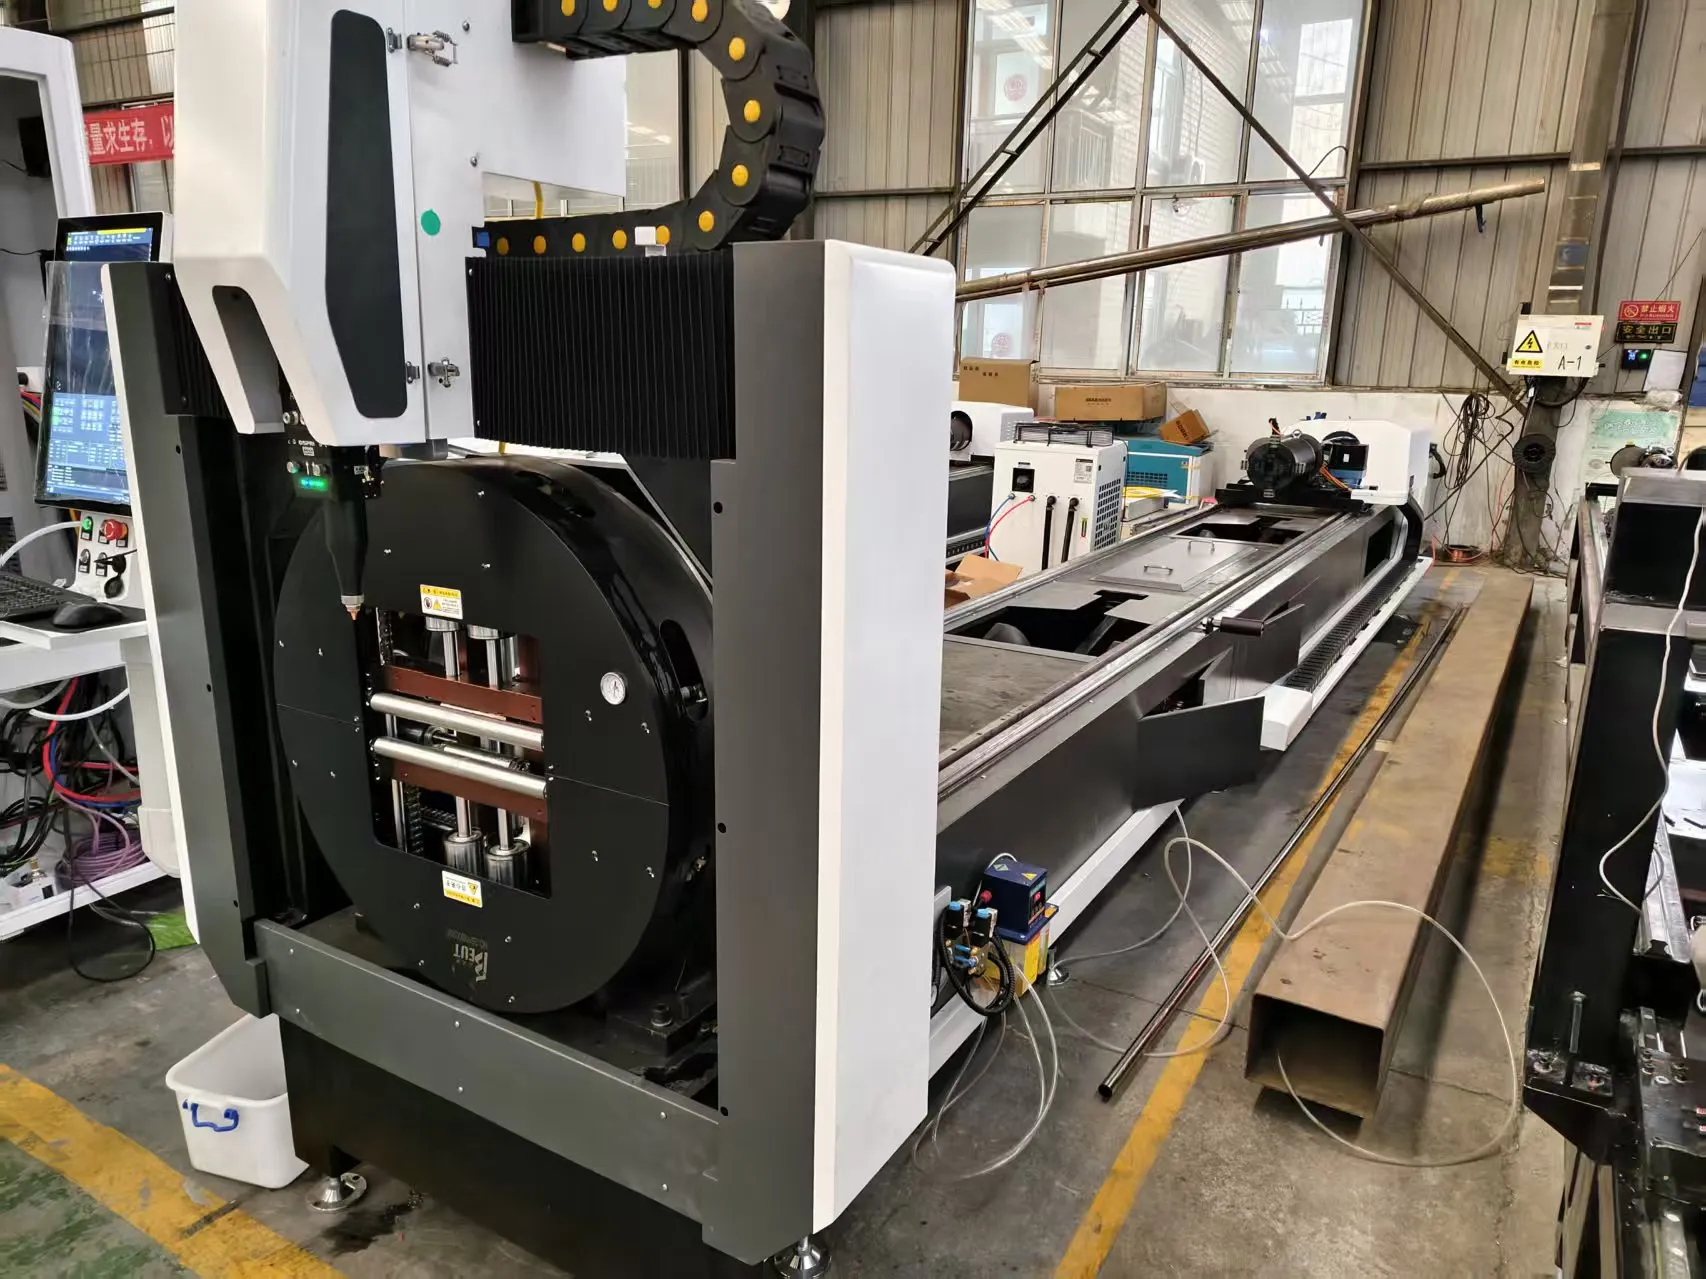
LT Series Tube Laser
Stainless tube Ø20-520 mm.
Compare all models →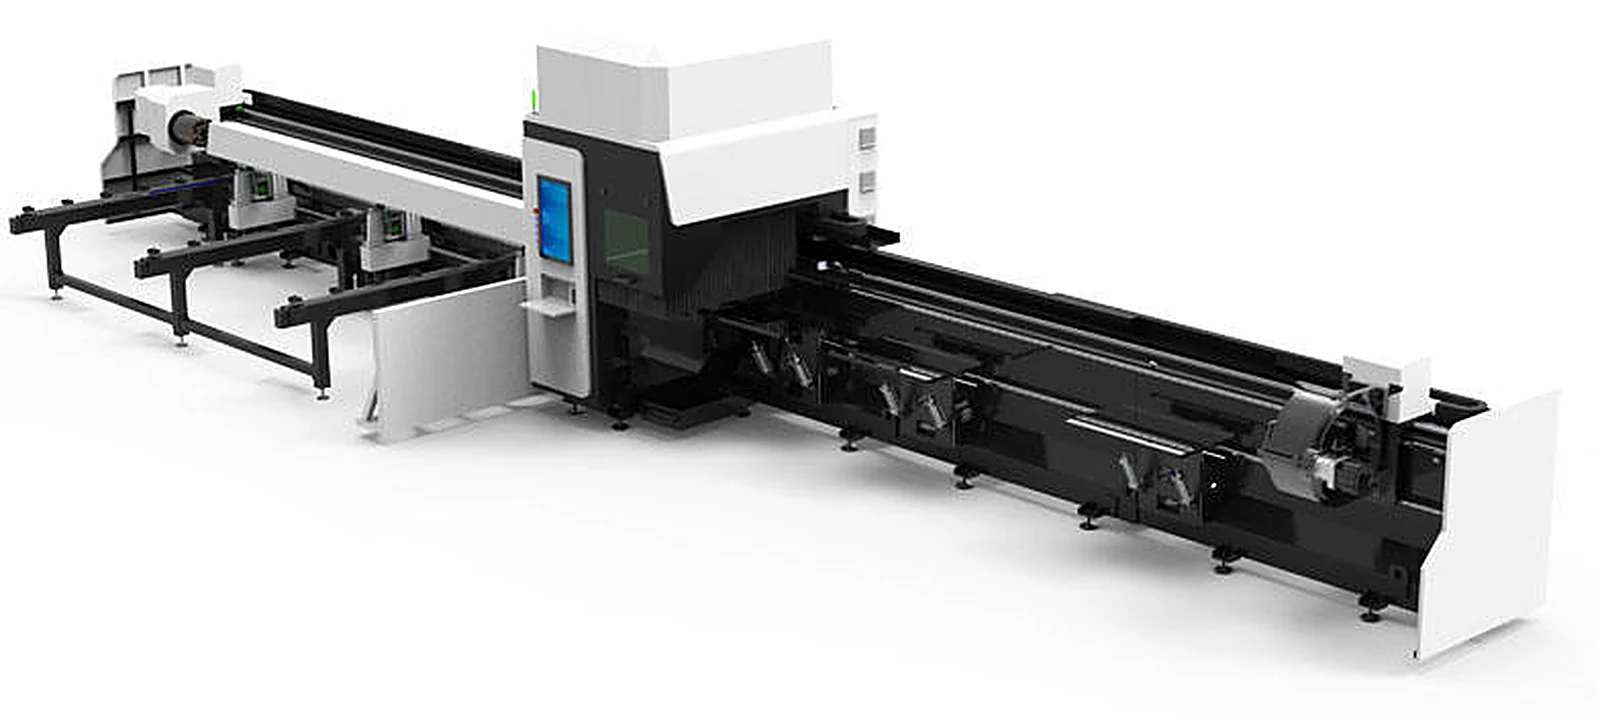
LT3 Three-Chuck Heavy Tube Laser
Zero tail on costly material.
View machine →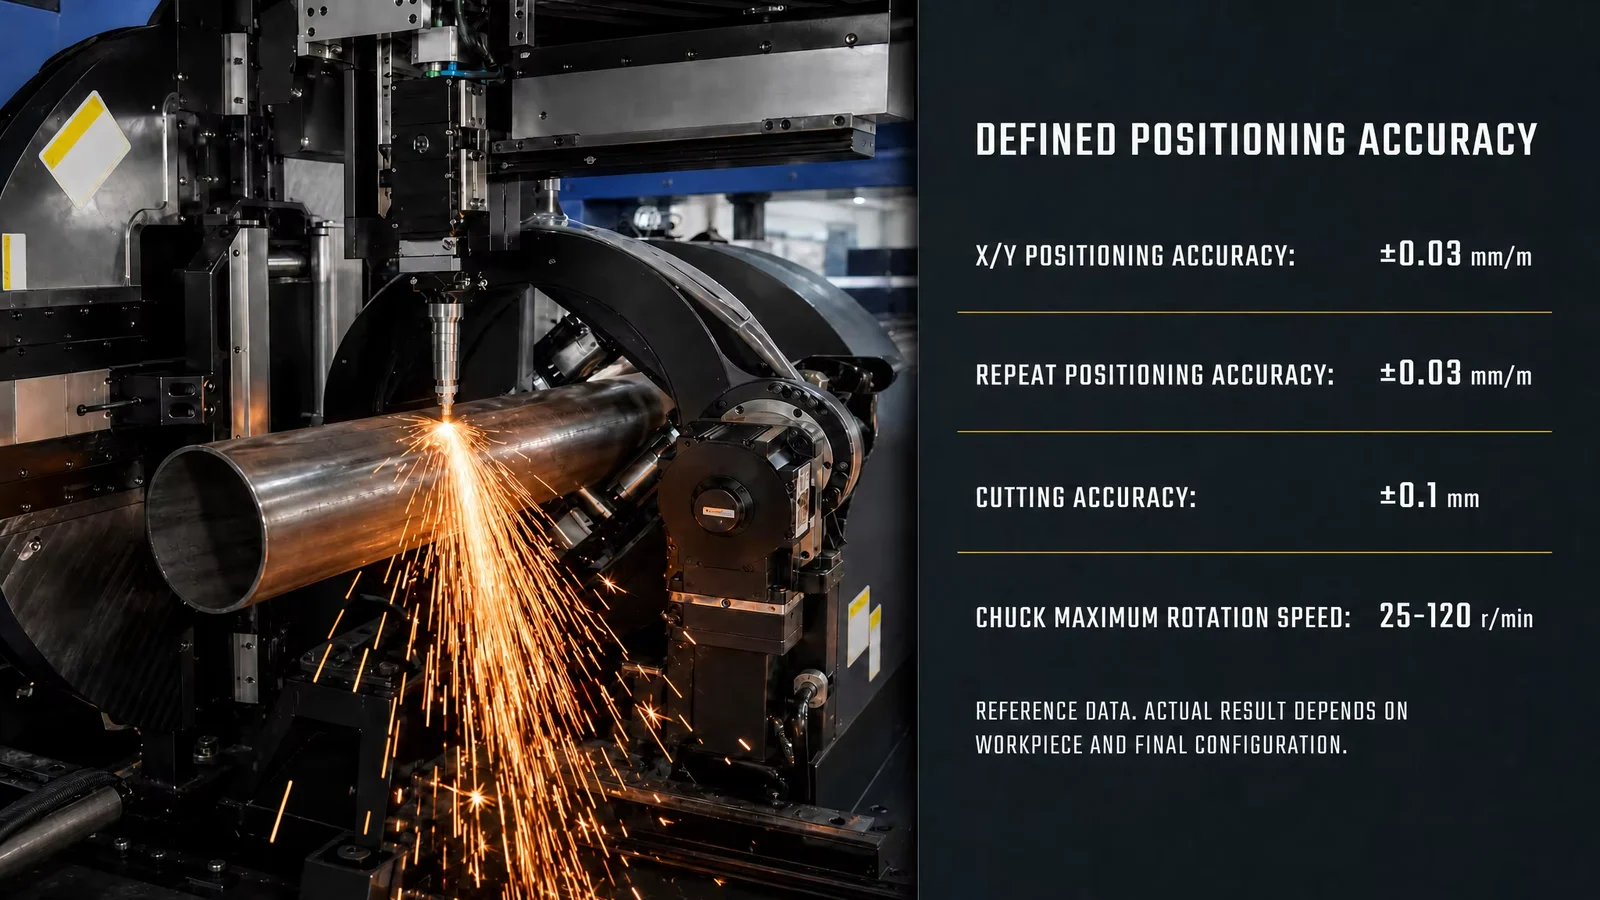
Round Tube Laser Cutting
Saddle fit-up and pipe sizes.
View machine →
Stainless Steel Laser Cutter
For stainless sheet and plate.
View machine →FAQ
Which gas is best for laser cutting stainless steel tube?
Nitrogen, for a bright oxide-free edge that can be welded or left visible. Compressed air is a lower-cost option for thin tube that will be painted.
How much nitrogen does a tube laser use?
It depends on nozzle size and pressure: about 13 Nm³/h for a 1.5 mm nozzle and 23 Nm³/h for a 2.0 mm nozzle at 12 bar, whenever the gas is on.
How do I calculate gas cost per metre?
Divide the flow in Nm³/h by the cutting speed in metres per hour and multiply by the gas price per Nm³.
Why are my stainless edges yellow or blue?
Oxygen is reaching the cut: low nitrogen purity, a leak in the gas line, or too little pressure. Check purity at the machine and the fittings first.
What nitrogen purity is needed?
99.99% or better for a bright edge. Lower purity shows as straw-coloured edges.
Can compressed air cut stainless tube?
Yes, on thin walls. The edge is slightly oxidised and greyer than with nitrogen, which is fine for parts that are painted.
Can a tube laser cut sanitary tube?
Yes. ASTM A270 and DIN 11850 tube is thin-wall and is cut with nitrogen on the LT240, with square, oxide-free ends for orbital welding.
Do laser cut stainless parts need passivation?
Nitrogen-cut edges keep their corrosion resistance; where a specification requires passivation after fabrication, ASTM A380 and A967 apply.
What laser power is needed for stainless tube?
1.5 kW for walls up to about 2-3 mm, 3 kW up to about 4 mm, 6 kW up to about 8 mm at production speed.
Is a three-chuck machine worth it for stainless?
Often yes: stainless costs several times more per metre than carbon steel, so zero tail waste pays back faster.