Discover the Advantages of Gantry Plasma Cutting Bevel Machine
PCL Group application engineering, Jinan · Updated 20 October 2026
Thick plates that are welded with full-penetration joints need a bevelled edge. A CNC plasma gantry with a bevel head cuts the part and its weld preparation in one pass, instead of cutting square and then grinding or milling the bevel by hand. This guide covers the bevel types, what the angle does to the cut, and how to get bevels that fit at the welding station.
On this page
What the angle does to the cut
A bevelled cut goes through more steel than the plate thickness. The length of the cut through the plate is the thickness divided by the cosine of the angle:
| Bevel angle | Cut length through the plate | 20 mm plate |
|---|---|---|
| 0° (square) | 1.00 × thickness | 20 mm |
| 15° | 1.04 × thickness | 20.7 mm |
| 30° | 1.15 × thickness | 23.1 mm |
| 45° | 1.41 × thickness | 28.3 mm |
So a 45° bevel on 20 mm plate needs the plasma power and speed of a 28 mm square cut. Cutting tables have to be set for the effective thickness, not the nominal one, or the bottom of the bevel will drag and leave dross.
Why bevel on the CNC instead of by hand
- One operation instead of two. The part comes off the table ready for fit-up; there is no grinding station behind the cutter.
- Consistent angle and root face. Welders get the same joint every time, which matters for weld procedures and for robotic welding.
- Contours, not only straight edges. Curved and variable bevels that are slow to grind are just another program.
- Less weld metal. An accurate bevel means a predictable joint volume, so less filler wire and shorter welding time.

Plasma, oxy-fuel or laser for bevels?
| Plasma | Oxy-fuel | Fiber laser | |
|---|---|---|---|
| Thickness | Thin to medium-thick plate | Thick to very thick carbon steel | Thin to thick; 5-axis heads on high-power machines |
| Materials | Carbon steel, stainless, aluminium | Carbon steel only | Carbon steel, stainless, aluminium |
| Edge | Clean bevel, light dross on thick plate | Oxide layer, needs cleaning | Narrow kerf, cleanest edge |
| Speed | Fast | Slow on thin plate, efficient on very thick | Fast on thin and medium plate |
| Machine cost | Medium | Lowest | Highest |
Many shops run a plasma bevel head and an oxy-fuel torch on the same gantry: plasma for most parts, oxy-fuel for the heaviest plate. For bevels on beams instead of plate, see beam bevel cutting.
Getting bevels that fit
- Calibrate the bevel head. Check the angle with a test cut at +45° and −45° and measure both; recalibrate after any torch crash.
- Set kerf and angle compensation. The kerf and the slight taper of the plasma arc change with angle, so bevel cuts need their own compensation values.
- Cut for the effective thickness. Use the cutting table for the cut length through the plate, not the nominal thickness.
- Control the root face. For Y bevels, the land is cut as a separate pass or a defined offset; check it with a gauge on the first part.
- Keep consumables fresh. A worn nozzle shows up first on bevel cuts as a wandering angle and dross at the root.
Machines
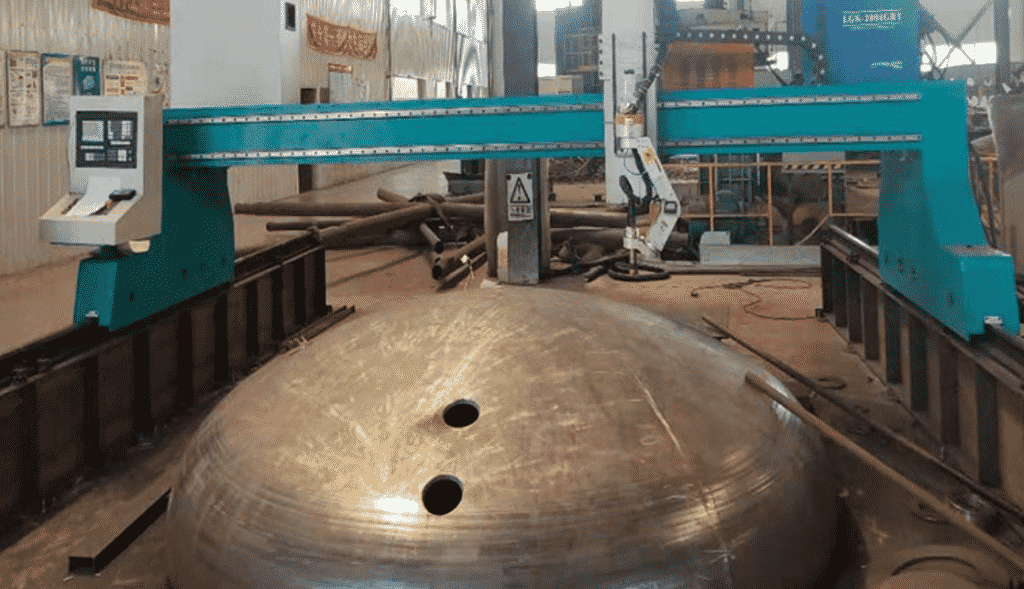
- Gantry CNC plasma cutting machine: widths 3 to 8 m, lengths up to 30 m, bevel head and oxy-fuel torches as options
- Gantry fiber laser for thin to medium plate with the cleanest edge
- HFT plate, tube and beam laser for bevels on plate, H-beams and tube
Common questions
What bevel angle can a plasma bevel head cut?
Up to 45° on PCL plasma bevel heads, for V, Y, X and K bevels and variable bevels along a contour.
Why does a bevel cut need more power than a square cut?
Because the cut goes through more steel: at 45° the cut length is about 1.41 times the plate thickness, so a 20 mm plate cuts like 28 mm.
Is plasma or laser better for weld bevels?
Plasma is the economical choice for medium to thick plate. A fiber laser gives a narrower kerf and cleaner bevel and is used where parts must fit without grinding.