Nitrogen vs Oxygen for Stainless Steel Fiber Laser Cutting
Assist gas affects how molten metal leaves the kerf, the appearance of the cut edge and the running cost of stainless steel fiber laser cutting. Nitrogen is commonly selected when a clean, low-oxidation edge is important. Oxygen or compressed air may be considered for specific machines and applications, but the correct choice depends on the material, thickness and required finish.
On this page
Quick answer: define the edge requirement first
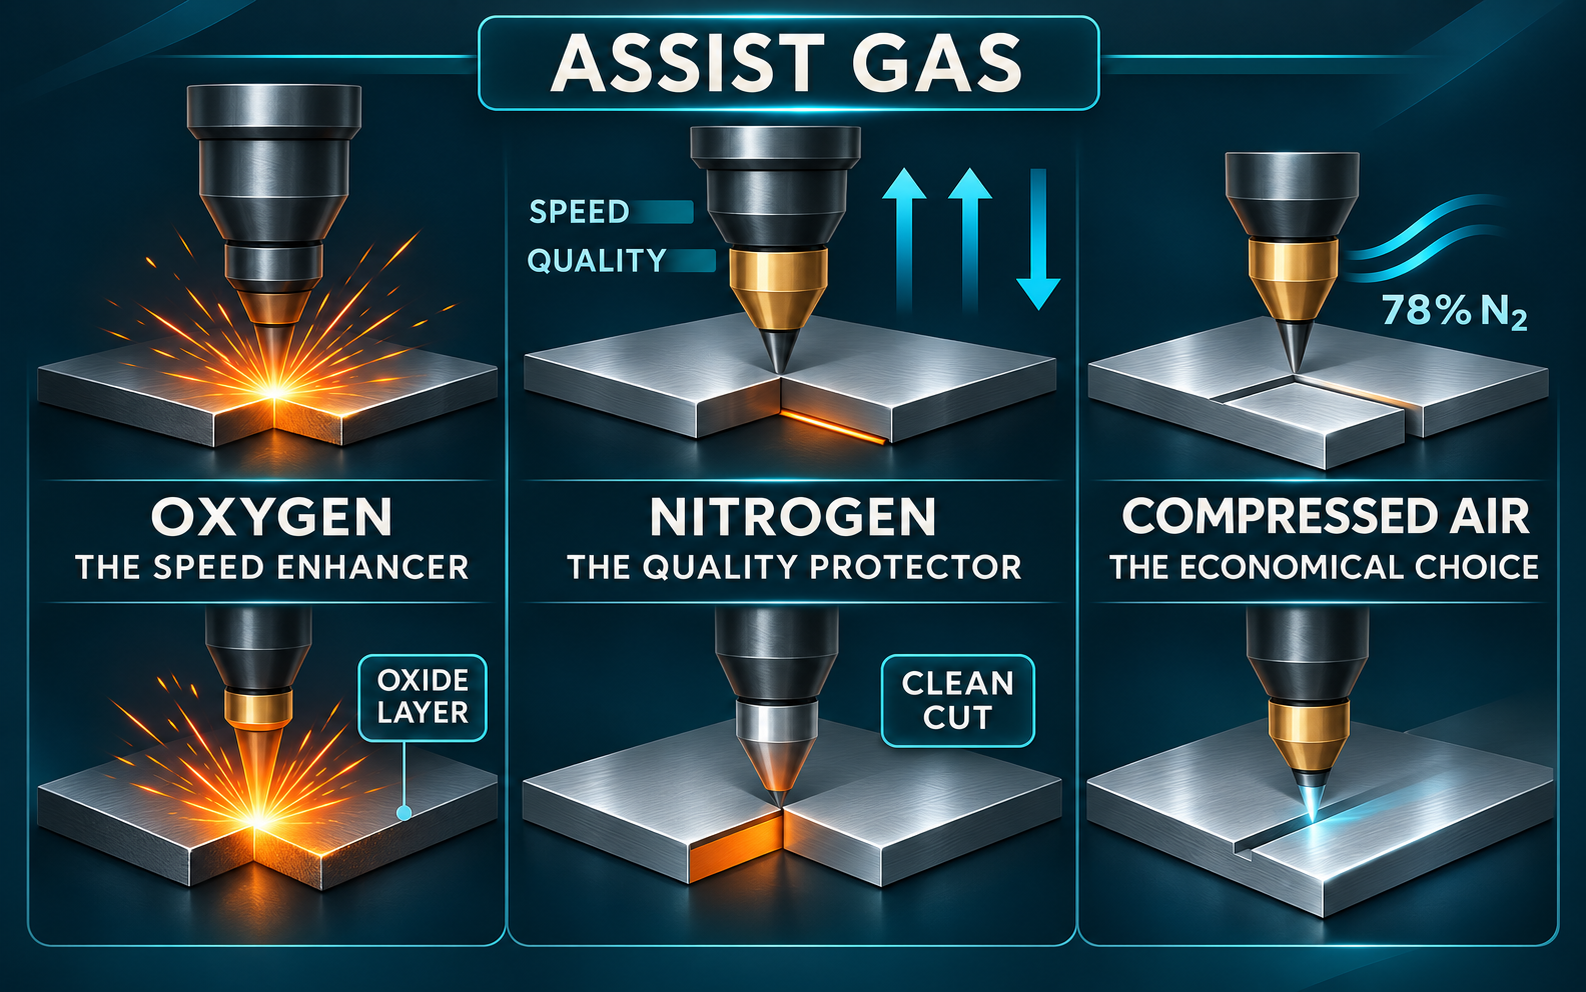
If the part will be painted, welded, polished or used as a visible surface, specify that requirement before choosing the assist gas. Nitrogen is often used when minimizing oxidation on stainless cut edges matters. Oxygen can create an oxide layer that may require additional finishing. Compressed air can be an option on some compatible systems, but it may change surface roughness and cut quality.
No gas choice guarantees the same result on every stainless grade, thickness and machine. Gas purity and pressure, nozzle, focus, speed, power, sheet condition and machine setup all affect the outcome. Use the manufacturer’s parameter chart as a starting point and validate it on a representative part.
Nitrogen, oxygen and compressed air compared
| Assist gas | Why shops evaluate it | What to inspect |
|---|---|---|
| Nitrogen | Often selected for stainless when edge appearance and low oxidation are priorities. | Gas purity, pressure, consumption, burr, dross and downstream finishing. |
| Oxygen | May suit certain process strategies and material conditions. | Oxide or discoloration on the edge, welding/coating requirements and cleanup. |
| Compressed air | May reduce gas-supply cost on compatible machines and applications. | Edge roughness, burr, material thickness and whether the quality specification allows the result. |
How assist gas affects edge quality
During laser cutting, the assist gas helps remove molten material from the kerf. With an inert gas such as nitrogen, the cut area is shielded from oxidation. When oxygen is used, it reacts with the material and can leave an oxide layer. That may be acceptable for some parts but undesirable when the edge must be painted, welded or left visible.
Compressed air may provide a lower-cost alternative in some thin-sheet applications, but it contains oxygen and other gases. The resulting edge finish must be checked against the application’s acceptance criteria. If a part will receive a coating or corrosion test, do not assume a visually acceptable edge will automatically meet the downstream requirement.
A practical test plan for stainless laser cutting
- Choose the stainless grade and thickness used in regular production.
- State the intended use: visible edge, weld preparation, paint, polish or another finish.
- Ask the supplier to test the recommended gas and settings on your drawing.
- Inspect the top and bottom edge, corners, small features, burr and discoloration.
- Record gas type, purity, pressure, nozzle, focus, speed and material condition.
- Compare total process cost, including gas, deburring, polishing and rework.
Common edge problems to investigate
| Observed issue | Items to review with the operator or supplier |
|---|---|
| Oxidized or discolored edge | Assist gas selection and purity, material surface, and the required finish after cutting. |
| Burr or dross underneath | Cutting speed, focus, nozzle condition, gas pressure and sheet flatness. |
| Rough or inconsistent cut face | Material variation, nozzle alignment, optics condition and parameter stability. |
| Results vary across the sheet | Sheet flatness, surface condition, protective film, focus and machine calibration. |
Nitrogen cost and total process cost
Nitrogen can have a higher gas-supply cost than oxygen or shop air, depending on the facility and supply method. But the gas price alone does not determine the lowest cost per finished part. If a different gas creates oxidation, extra grinding or rejected parts, those steps also belong in the calculation.
Compare gas consumption, cutting time, edge acceptance, secondary operations and scrap using the same sample job. A production test is more useful than comparing a machine’s maximum speed or a single idealized cut.
See the PCL stainless laser cutting machine page for the stainless-focused machine information. Include your grade, thickness, drawing and edge-finish requirement when requesting a test or quotation.