Gantry Fiber Laser Cutting Machine for Large Steel Plates
Plate laser for long parts
A gantry fiber laser built for full mill plates. The bridge spans the bed and runs its whole length, so a 3 × 12 m plate goes on in one lift and comes off as finished parts: girder webs, bridge plates, stiffeners and base plates cut to ±0.03 mm.
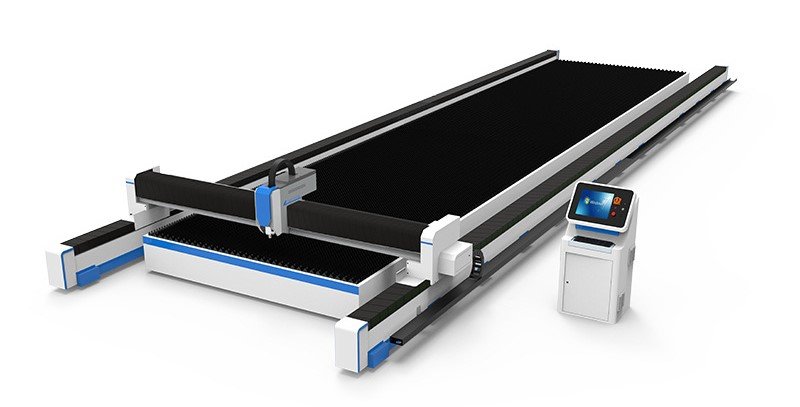
- Working length
- 12 m
- Laser power
- 1–30 kW
- Positioning
- ±0.03 mm
- Acceleration
- 1.5 G
- Source
- Maxphotonics
See it cutting

The gantry laser cutting steel plate in the PCL workshop.
What is inside

Aviation aluminium beam
The bridge is a single aluminium extrusion pressed on a 4,300-ton line, then aged and solution-treated so it holds its shape. Aluminium carries the cutting head with far less mass than a welded steel beam, which is what lets the machine reach 1.5 G without the bed shaking.
On long plates this matters every minute: most of a gantry laser’s time on small parts is spent accelerating and braking, not cutting.

Drive on both sides
A rack-and-pinion drive runs on each side of the bed and the two motors are synchronised, so the bridge stays square even at full acceleration. High-precision linear guides carry the load, and lubrication is automatic.
Single-side drives are cheaper, but on a 12 m bed they let the far end of the bridge lag; holes at the edge of the plate drift out of position.

Fiber source and auto-focus head
Maxphotonics is fitted as standard, with Raycus or IPG on request, from 1 kW to 30 kW. The auto-focus head sets focus for each material and thickness from the cutting table, so changing from 3 mm stainless to 20 mm carbon steel is a program change, not a manual adjustment.
The control nests parts, plans the cutting path and uses leapfrog moves between parts to cut idle time. Drawings come in as DXF or PLT.

Welded, stress-relieved bed
The bed is welded carbon steel, annealed after welding to remove the stresses that otherwise make a long bed creep in its first year. It is hollow and split into extraction zones: only the zone under the head opens, so suction stays strong over a 12 m length.
Heavy plates go onto the fixed bed by crane or vacuum lifter, and the slats can be replaced section by section as they wear.
Specifications
- Working length
- up to 12,000 mm
- Plate sizes
- 3 × 8 m, 3 × 12 m, others to order
- Laser power
- 1 to 30 kW
- Laser source
- Maxphotonics; Raycus or IPG
- Positioning accuracy
- ±0.03 mm
- Maximum acceleration
- 1.5 G
- Drive
- Dual rack and pinion, synchronised
- Guides
- High-precision linear guides
- Lubrication
- Automatic
- Cutting head
- Auto-focus
- Software
- Nesting, path planning, leapfrog
- File formats
- DXF, PLT
- Bed
- Welded, annealed, hollow
- Extraction
- Partitioned zones
Bed length, power and options are configured to your plates. Send your largest plate and thickest material and we confirm the configuration.
How thick it cuts
The thickest plate each source cuts in continuous production, from the cutting data of Maxphotonics. A source can cut through more than this, but not stably enough for series work.
Carbon steelStainless steel · production thickness, Maxphotonics data
For speed, gas, focus and nozzle at every thickness, see the fiber laser cutting speed chart. For 20 kW and above, see high-power fiber lasers.
Where the gantry pays off
Planning the installation
A gantry laser is a building project as much as a machine purchase. The bed sits on a level concrete foundation laid to our drawing, and the crane has to cover the full length so plates can be placed and skeletons lifted out. Power, a chiller, an air compressor and the gas supply are sized to the laser source, and the extraction duct needs a route out of the building. We send the layout and foundation drawing with the quotation and train your operators during commissioning. The full checklist is in how to choose a gantry laser for large plates.
Gantry laser or something else?
| Your work | Better fit |
|---|---|
| Plates longer than about 6 m, or full mill plates | Gantry laser |
| Mostly 3 × 1.5 m or 4 × 2 m sheets | Enclosed sheet laser with exchange table |
| Thick plate where edges are ground anyway, lowest machine cost | Gantry plasma |
| H-beams, channels and tube as well as plate | HFT plate, tube and beam laser |
FAQ
How long a plate can the PCL gantry laser cut?
Working lengths go up to 12,000 mm, so full 3 x 12 m plates are cut in one load.
What laser power is available?
1 kW to 30 kW. Maxphotonics is standard; Raycus or IPG can be fitted on request.
How accurate is it over a 12 m bed?
Positioning accuracy is ±0.03 mm, with a dual synchronised rack-and-pinion drive and a stress-relieved bed.
How thick can it cut?
In continuous production, a 12 kW source cuts carbon steel up to 35 mm and stainless steel up to 25 mm. Higher powers cut thicker plate.