12–30 kW H-Beam Laser Cutting Machine for Structural Steel

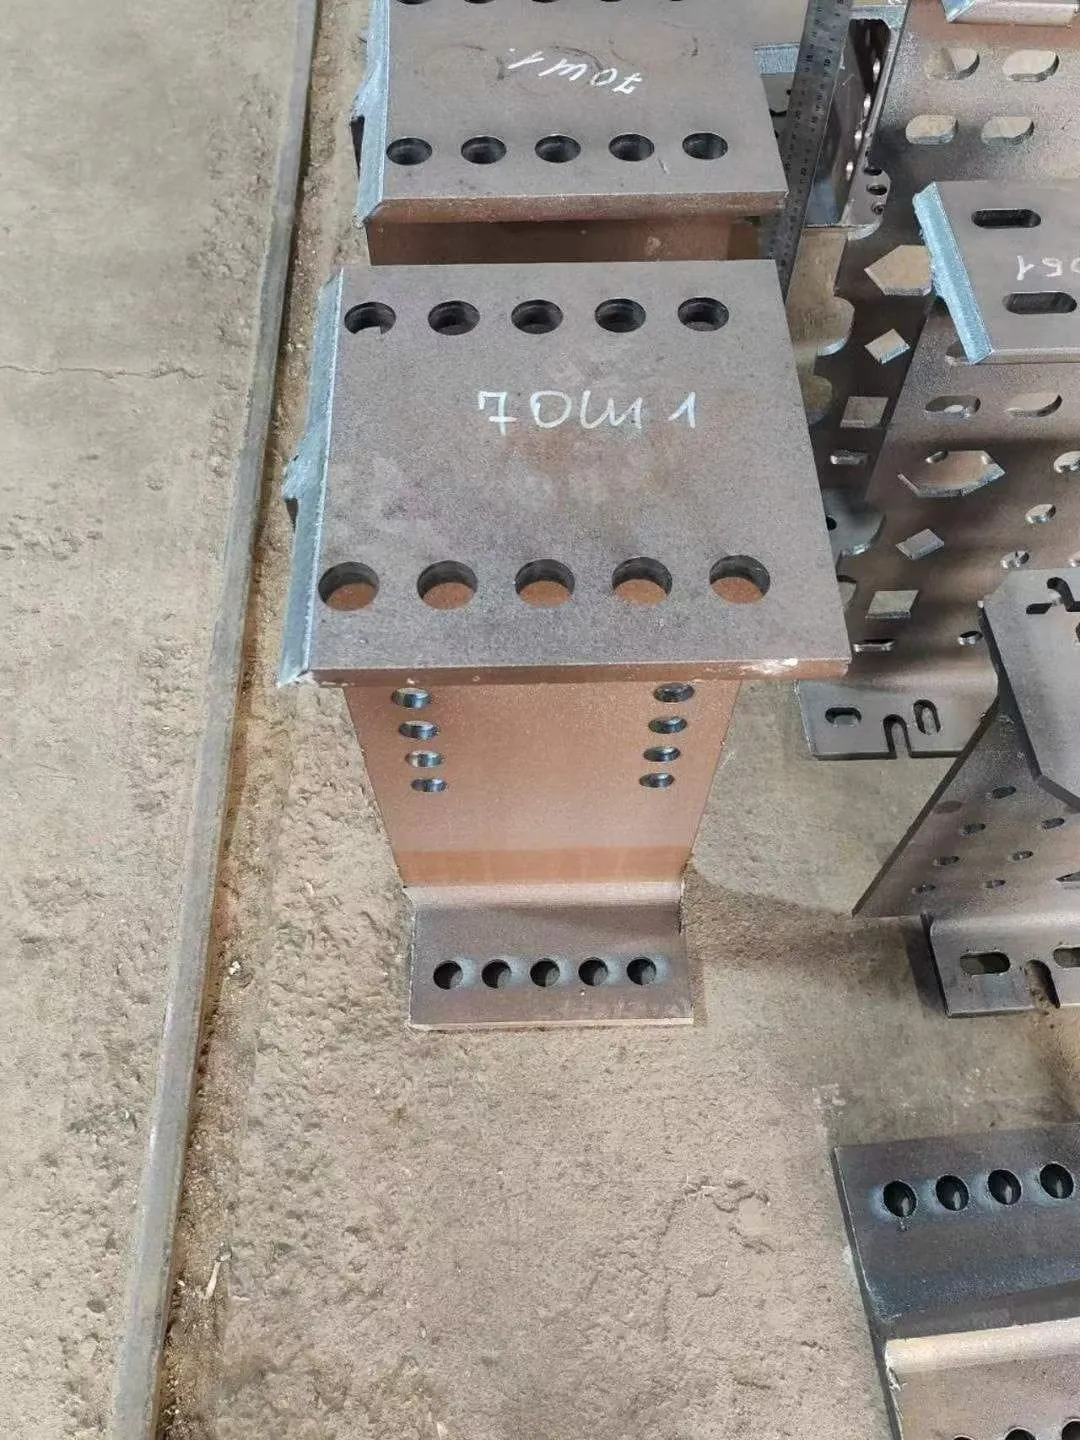
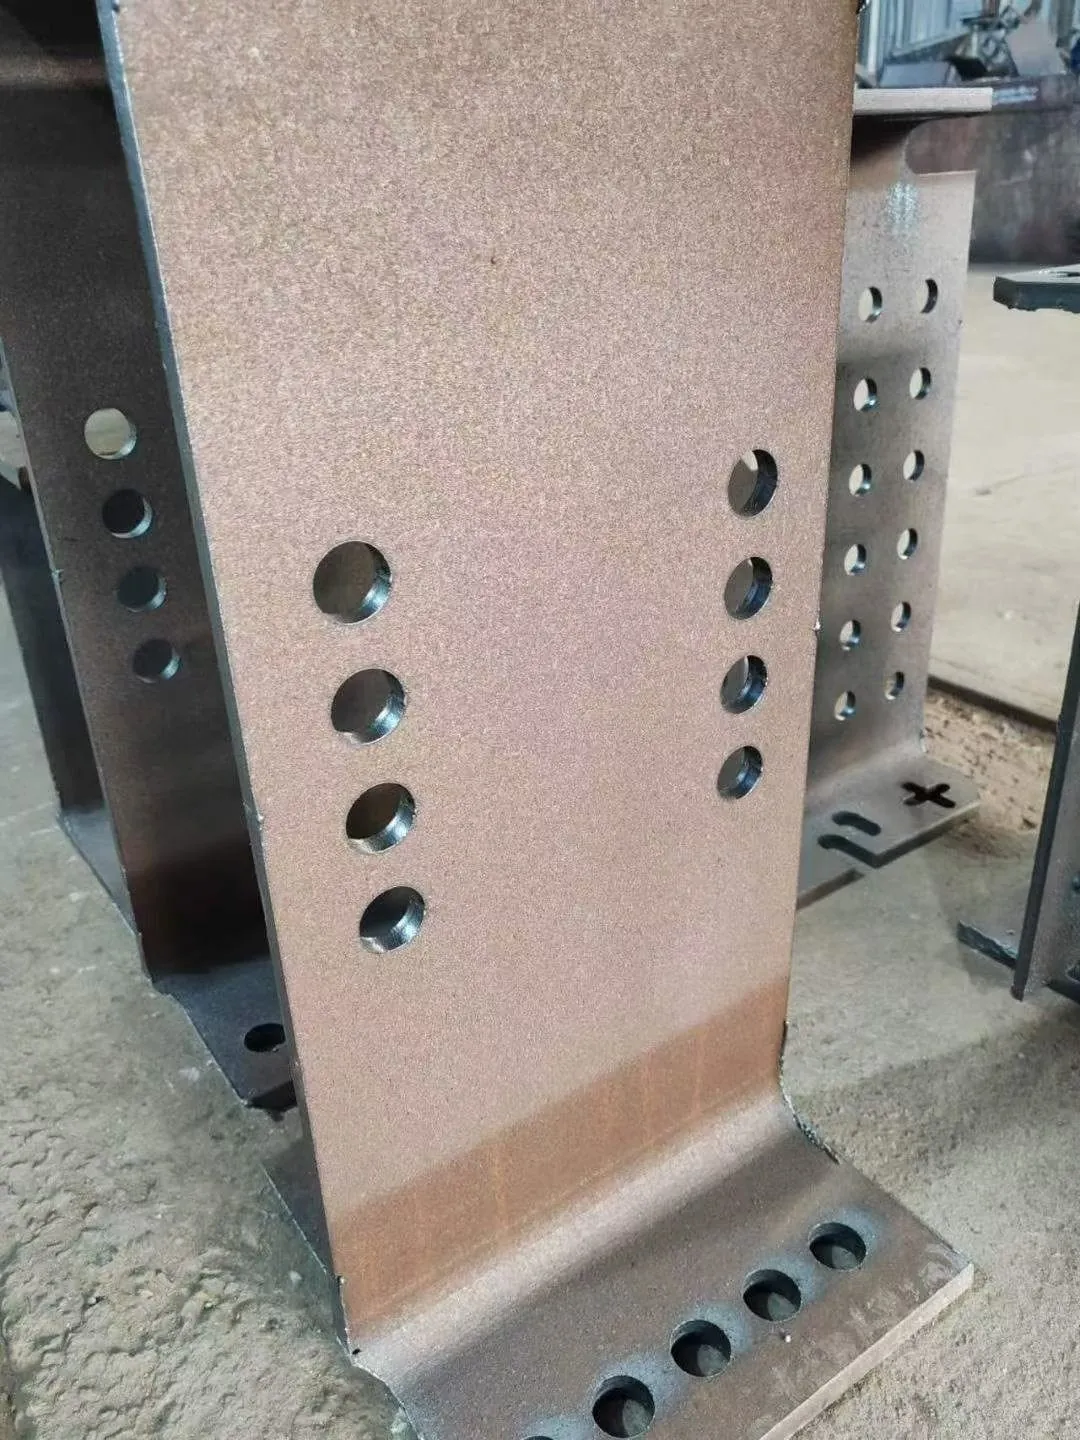
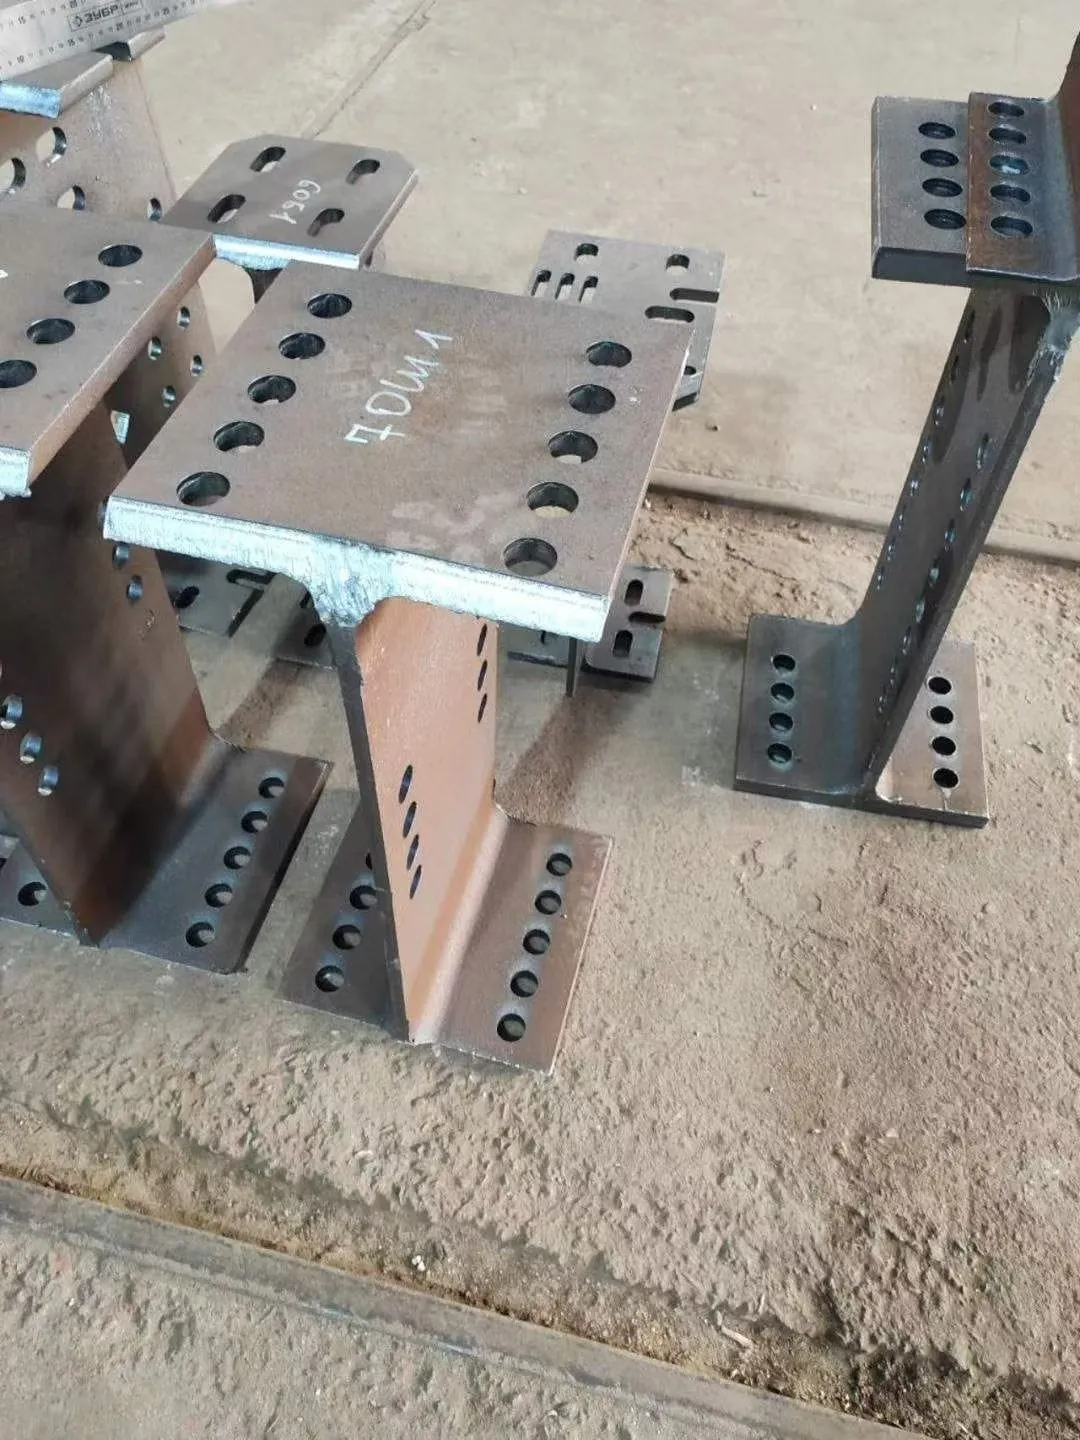
12, 20 or 30 kW 5-axis fiber laser cuts H-beams, I-beams, channels and angles up to 1,000 mm high and 12 m long, and cuts to length, copes, weld access holes, ±45° bevels, bolt holes and layout marks in a single setup. The beam is never clamped in a chuck, so the last part is cut to the end of the bar with no tail-end offcut.
At a glance
- 12, 20 or 30 kW fiber laser; the 20 kW model cuts up to 40 mm carbon or stainless steel.
- Sections up to 1,000 mm high (HEA and HEB 1000, W-shapes to about 39 in, UB 914); angles up to 800 mm leg.
- 5-axis TCP head: A axis 360°, C axis 180°, V/Y/K bevels to ±45°.
- Zero-remnant cutting: 0 mm tail, against 100–300 mm on chuck machines.
- Tekla DSTV, IGES and STEP files cut directly, with part numbers marked.
What it cuts
The machine is built for the open sections that make up most steel frames. Any rolled or welded H-section up to 1,000 mm high fits on the bed, whatever standard it is rolled to.
- European sections: HEA and HEB wide-flange beams up to the 1000 size, HEM up to 900, and every IPE I-beam and UPN channel.
- American sections: W-shapes (wide-flange) up to about 39 in (1,000 mm) deep, plus S-beams and C-channels.
- British sections: UB and UC universal beams and columns, PFC channels.
- Chinese sections: HW, HM and HN hot-rolled H-sections, and welded H-beams from a beam assembly and welding line.
- Angles: equal and unequal angles up to 800 mm leg length.
Dimensions, weights and naming for every common section are in the steel beam size chart, which also shows whether a size fits this machine. Channel, angle and I-beam cutting uses the same program logic as H-beams.
Every process in one setup
The beam is loaded once. The machine calibrates the actual position of the section, since rolled beams are never perfectly straight, and then runs the whole part program.
| Process | What the laser does |
|---|---|
| Cut to length | Square or mitred ends on web and flanges, including the last part on the bar. |
| Beam coping | Notches and cope cuts for beam-to-beam and beam-to-column connections. |
| Weld access holes | Radiused rat holes cut in one continuous path, with no start-stop notch. See weld access holes and beam coping. |
| Weld bevels | V, Y and K bevels up to ±45° on flanges and web. |
| Bolt and slotted holes | Round and slotted holes in web and flanges in place of drilling. Background in laser cutting bolt holes in steel structures. |
| Layout marking | Part numbers and assembly lines marked by the laser for fit-up and traceability. |
All of this depends on the 5-axis head keeping the beam on its tool centre point while it tilts around the flange. How TCP control works on H-beam cutting covers the motion in detail.
Zero-remnant cutting
Profile lasers with a chuck have to grip the bar while they cut, and the gripped length ends up as scrap, usually 100 to 300 mm per bar. This machine works the other way round: the beam rests on the bed and the cutting head moves along it, so nothing holds the end and the last part is cut right to it.

Video: cope, access hole and bevel, then the last part cut to the bar end.
| Steel lost per 12 m bar | Chuck machine 100 mm tail | Chuck machine 300 mm tail | PCL H-beam laser |
|---|---|---|---|
| HEA 300 88.3 kg/m | 8.8 kg | 26.5 kg | 0 kg |
| HEB 600 212 kg/m | 21.2 kg | 63.6 kg | 0 kg |
Across 1,000 bars of HEB 600, a 300 mm tail adds up to 63.6 t of steel.
Specifications
| Item | Specification |
|---|---|
| Laser power | 12 kW, 20 kW or 30 kW fiber laser |
| Laser source brand | Maxphotonics as standard; Raycus or IPG on request |
| Cutting thickness | carbon steel and stainless steel up to 40 mm on the 20 kW configuration; see the power guide below |
| Cutting head | 5-axis TCP head, A axis 360°, C axis 180°, water cooled, auto focus |
| Bevel | ±45°; V, Y and K bevels |
| H / I beams and channels | section height up to 1,000 mm |
| Angles | leg length up to 800 mm, 1,000 mm on request (most orders are under 300 mm) |
| Effective cutting width / length | 2,500 mm / 12,000 mm |
| Machine footprint (W × L) | 3,500 mm × 14,000 mm |
| Cutting speed / rapid traverse | 0–3,500 mm/min / 0–15,000 mm/min |
| Cut surface roughness | Ra 2.5–25 µm |
| Drives | Japanese servo motors, SHIMPO reducers, PEK linear guides, LEITESEN racks |
| Control and files | NC-studio; imports Tekla DSTV (.nc), IGES and STEP; works with AutoCAD and SolidWorks |
| Warranty | 3 years on the machine, 2 years on the laser source |
Longer beds and other section ranges can be configured. Tell us your thickest flange and longest bar when you ask for a quote.
Choosing 12, 20 or 30 kW
| Power | Typical work | Why choose it |
|---|---|---|
| 12 kW | Light frames, purlins, small H-beams and channels with mostly thin flanges | Lowest investment and running cost |
| 20 kW | General steel structures, buildings, warehouses, bridges; flanges up to 40 mm | The standard balance of thickness, speed and cost |
| 30 kW | Heavy sections and high tonnage, many thick flanges per shift | Faster cutting on thick flanges, more parts per day |
The bed, section range and software are the same for all three power levels.
Laser, plasma or saw and drill line
We build all three types of beam equipment, so the choice comes down to the parts you make. In short: a drill line suits plain holes and square cuts, plasma suits heavy cutting on a budget, and the laser suits fabricators who need copes, access holes, bevels and holes finished to fit-up without rework.
| H-beam fiber laser | CNC plasma beam cutter | Saw and drill line | |
|---|---|---|---|
| Copes and access holes | Yes, one continuous path | Yes, wider kerf and larger heat-affected zone | Needs a separate coping machine |
| Weld bevels | V / Y / K to ±45° | Yes, with a bevel torch | No |
| Bolt holes | Cut, including slotted holes | Cut, with more taper | Drilled |
| Marking | Laser marking | Plasma marking | Scribing unit, if fitted |
| Tail-end offcut | 0 mm | Depends on clamping | Depends on clamping |
| Rework after cutting | Little or none | Grinding often needed | Copes and bevels done elsewhere |
For a broader view of cutting methods, see cutting methods in steel structure construction.
Software and files
Parts come straight from the detailing model. The controller imports Tekla DSTV (.nc) files, IGES and STEP, and works with drawings from AutoCAD and SolidWorks, so copes, holes and marks are not re-drawn at the machine. Part numbers are marked on the steel for assembly.
Projects
Customer sites, in the order the videos were published. Customer names are not shown.

Bridge fabricator, China
H-beams for a steel bridge project cut on site at the fabricator’s plant.

Steel structure plant, China
One laser line cutting both H-beams and steel plate for a structural steel plant.

Cutting to robotic welding, China
Beams cut on the H-beam laser, then welded on a PCL AGV robotic welding cell. More
After cutting, beams can go straight to welding. See the teaching-free robotic welding station and the AGV mobile welding robot.
Questions
What is the largest beam the machine can cut?
H-beams, I-beams and channels up to 1,000 mm section height and 12 m effective cutting length. That covers HEA and HEB up to the 1000 size, HEM up to 900, every IPE and UPN size, W-shapes up to about 39 in deep and UB sections up to 914 mm. Angles go up to 800 mm leg length.
How thick can the laser cut on a beam?
The 20 kW configuration cuts up to 40 mm in carbon steel and stainless steel. 12 kW suits lighter sections, and 30 kW cuts thick flanges faster. Most rolled H-beam flanges are well inside that range; only jumbo column sections such as the heavier W14 and HD shapes have flanges thicker than 40 mm.
Can laser-cut holes replace drilled bolt holes?
For most connection holes within the 40 mm thickness limit, yes, and slotted holes are cut in the same pass. Hole size limits and edge requirements for slip-critical joints are set by the project specification, so check them before removing drilling from the process.
Why is there no tail-end offcut?
The beam lies on the bed and the cutting head travels along it. Nothing clamps the end of the bar, so the last part is cut to the end. Chuck-type profile lasers have to hold the bar and usually leave 100 to 300 mm per length.
Does the machine meet EN 1090?
EN 1090-2 certifies the fabricator’s factory production control, not a single machine. The laser supports it with part marking for traceability and a consistent cut surface (Ra 2.5 to 25 µm). Compare the cut quality class required in your execution specification with test cuts on your own sections.
Which laser sources can be fitted?
The machine takes a 12 kW, 20 kW or 30 kW fiber source. Maxphotonics is standard; Raycus and IPG are available on request. Power and source brand change the configuration and the price, so tell us your thickest flange when you ask for a quote.
Should I choose 12 kW, 20 kW or 30 kW?
Choose by your thickest flange and your daily tonnage. 12 kW suits light frames with mostly thin flanges, 20 kW is the standard choice for general steel structures, and 30 kW suits heavy sections and high output, where cutting speed on thick flanges matters most.
What warranty comes with the machine?
Three years on the machine and two years on the laser source.
Ask for a cutting trial
Send a drawing or DSTV file with the material, largest section and monthly tonnage. We cut a sample part, send you the video and recommend a configuration. PCL Group has built cutting machines in Jinan, China since 2005, and the machines carry CE and FDA certification.
Related machines
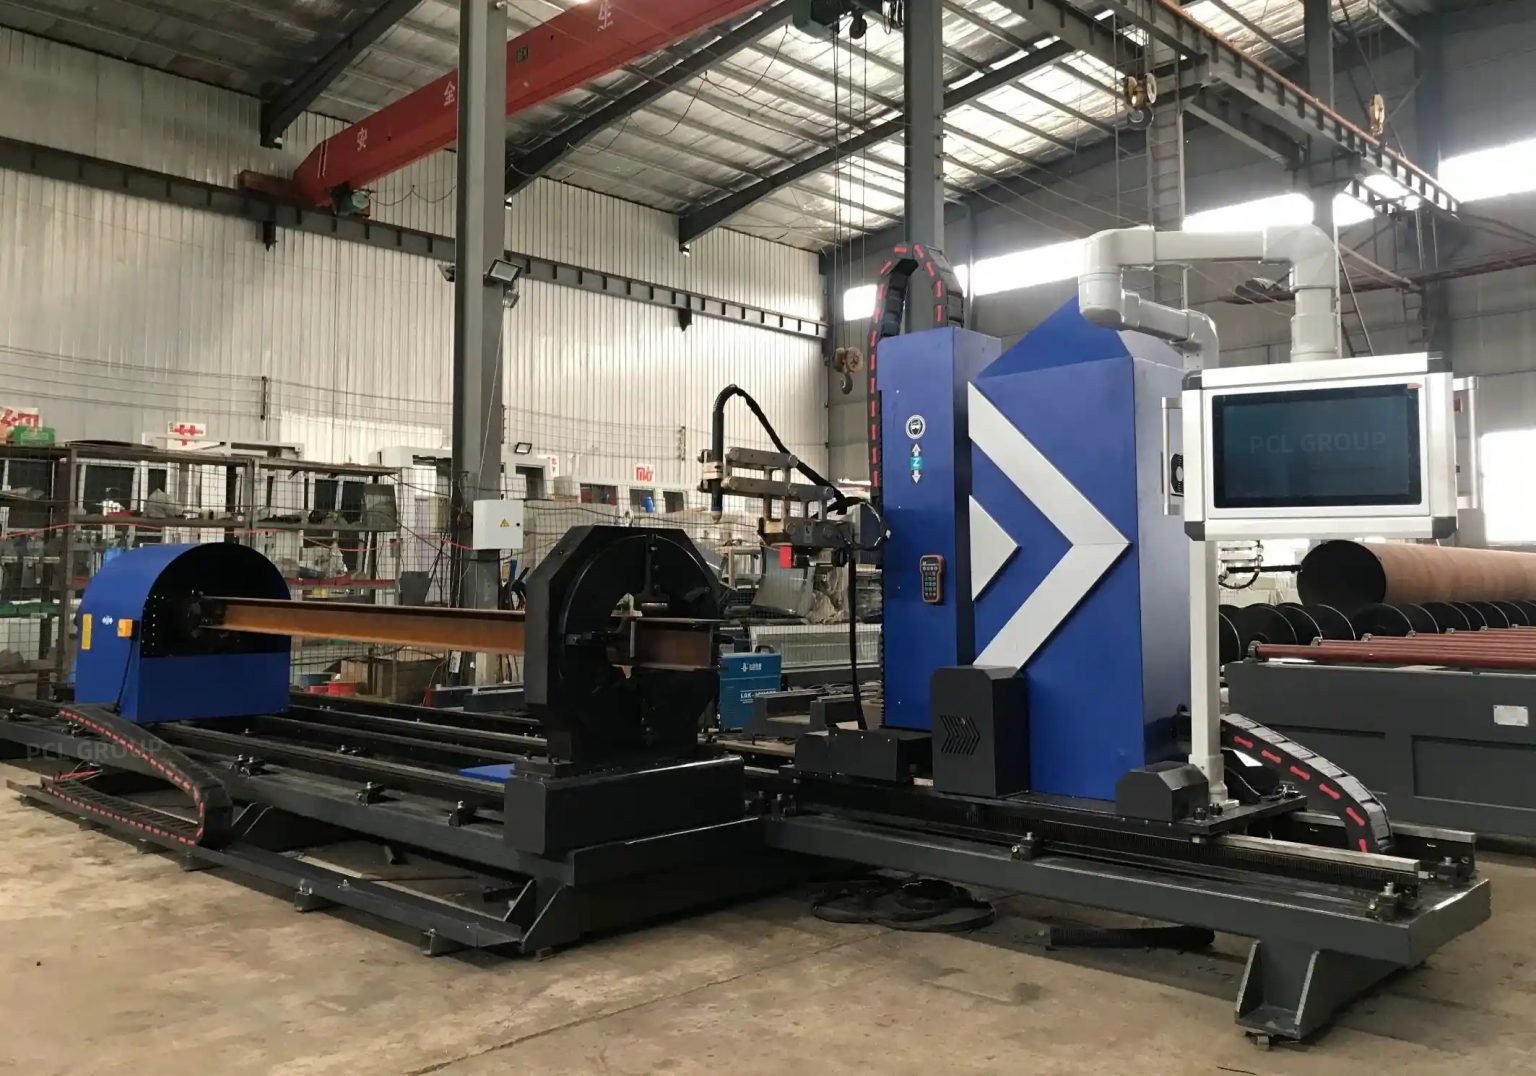 8-Axis CNC Plasma Beam Cutter8-axis plasma for copes, bevels and holes on H-beams, box and pipe.View machine →
 H-Series Robotic Beam Cutter6-axis robot plasma for copes, bevels and holes.View machine →
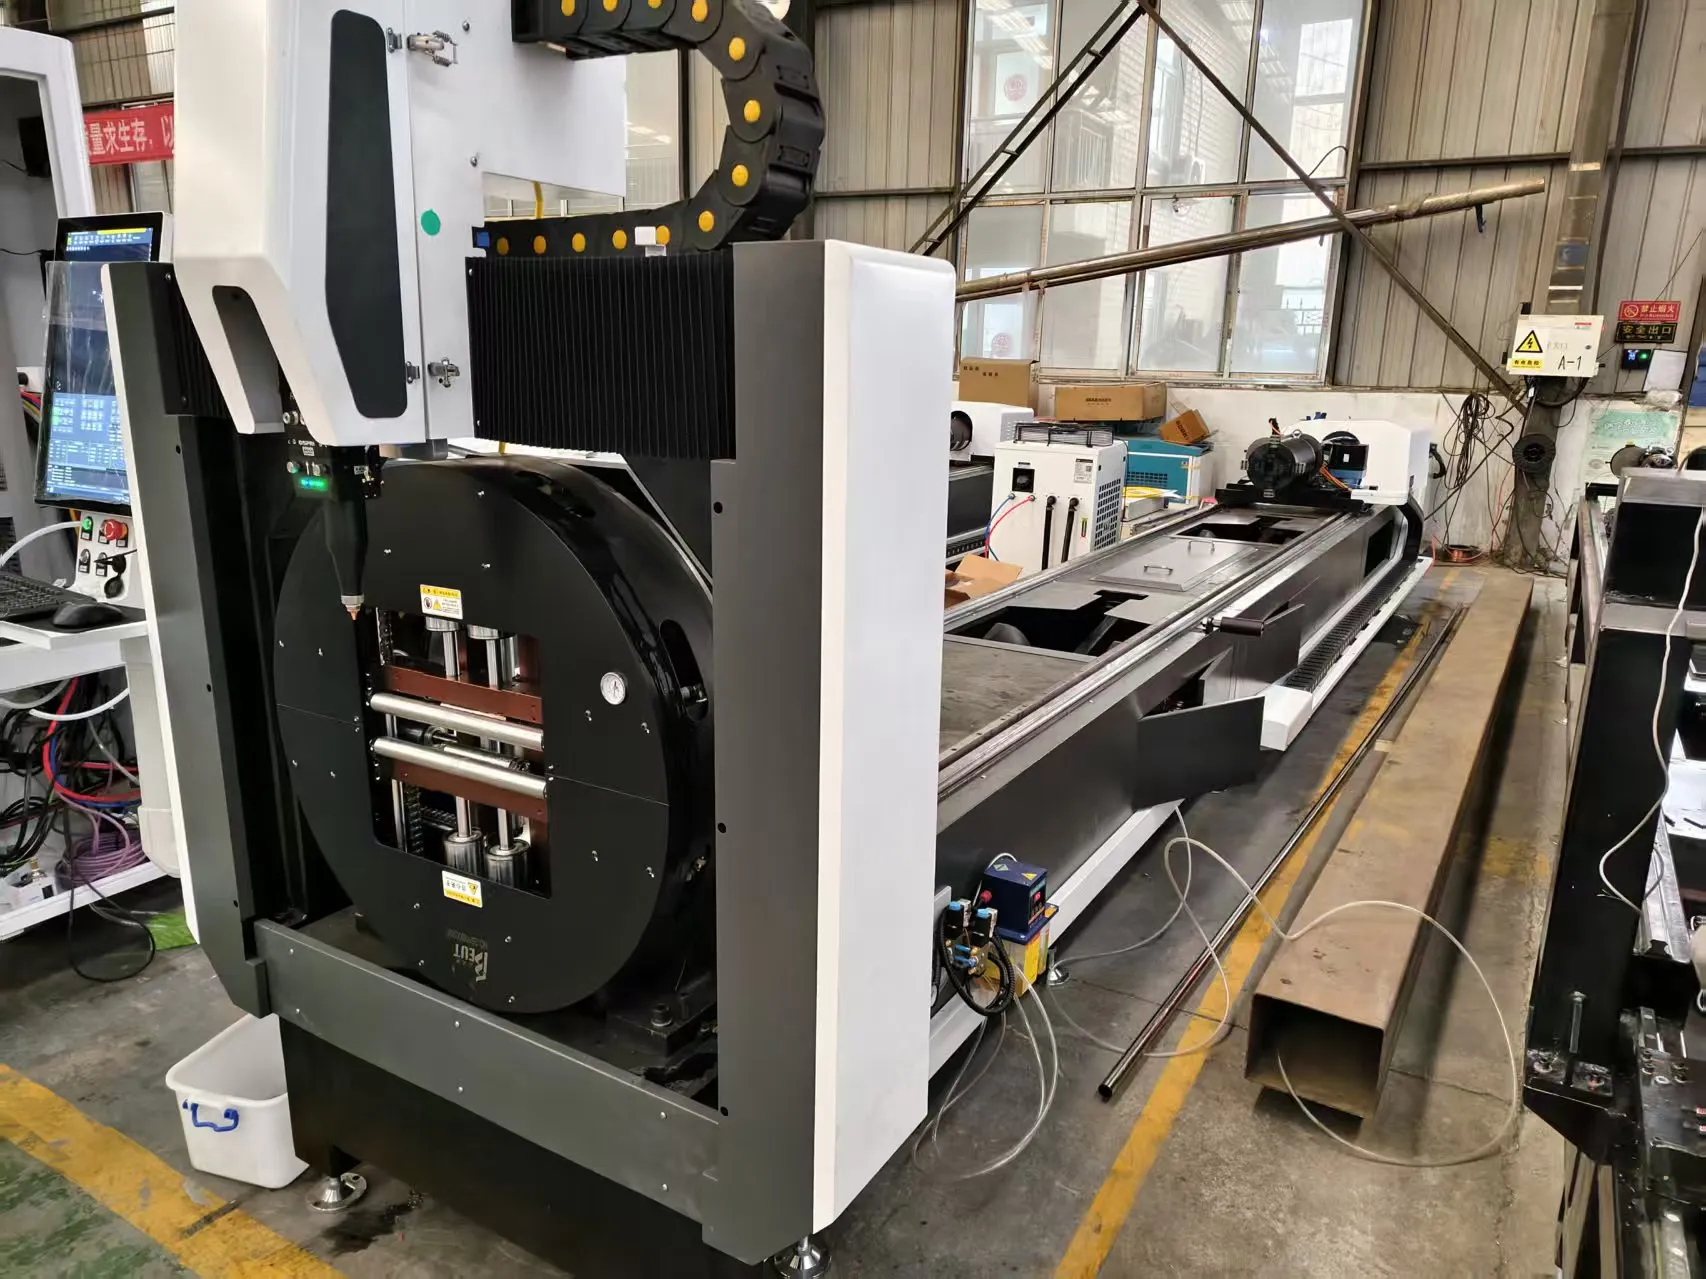 Tube Laser LT240Round, square and rectangular tube with chuck feeding.View machine →
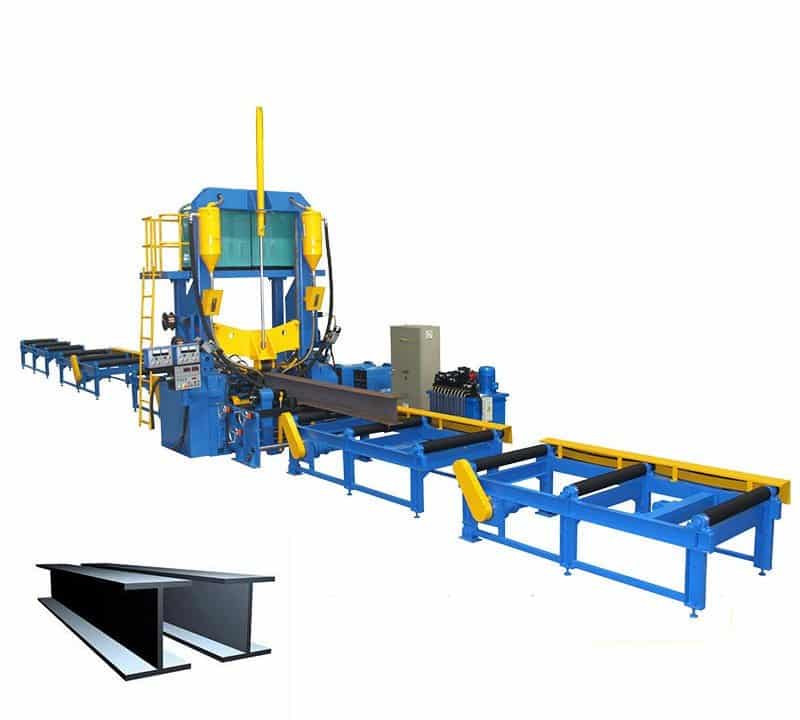 H-Beam Production LineAssembly, welding and straightening of welded H-beams.View machine →
 Teaching-Free Welding StationRobot welding of beams and columns without programming.View machine →
 AGV Welding RobotMobile robot that welds large structures in place.View machine →