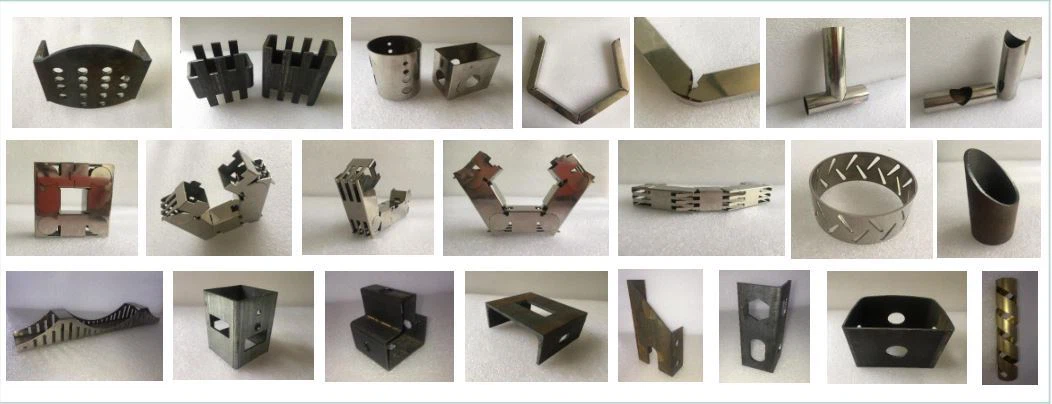
Severe Workshop Condition Adaptation, Thermal Expansion Mitigation, and Stress-Relieved Bed Stability in Stainless Tube Laser Cutting
Locomotive hydraulic lines are not a cosmetic application. They are pressure-bound arteries carrying 200–350 bar of phosphate-ester or mineral-based hydraulic fluid through a chassis that flexes, vibrates, and thermally cycles from -40°C yard staging to 70°C+ engine-room soak. When a maintenance depot specifies stainless steel tube laser precision for locomotive hydraulic lines, the decision is driven less by cut aesthetics and more by fatigue life at the weld collar, ovality retention at the flare seat, and repeatable kerf geometry across a 6-meter tube run. That is a machine-tool stability problem before it is ever a laser problem.
The dominant alloy in this segment is SUS304 (ASTM A312 TP304) in 12–25 mm OD, 1.5–3.0 mm wall, with occasional SUS316L for coastal rail corridors. Yield strength sits near 215 MPa annealed, thermal conductivity is roughly 16.2 W/m·K — about one-third that of carbon steel — and the coefficient of thermal expansion runs 17.3 µm/m·°C. That low conductivity is the root cause of most field failures in tube laser cells: heat does not evacuate down the tube axis, it accumulates at the cut zone and migrates into the chuck jaws and the bed structure.
Why Conventional Methods Fail on Hydraulic Line Geometry
Plasma and abrasive sawing remain in legacy depots because they are cheap to buy. They are expensive to own. Plasma on 2.0 mm SUS304 produces a heat-affected zone of 0.4–0.9 mm with chromium depletion at the grain boundaries, which becomes an intergranular corrosion initiation site once the line sees chloride-laden brake dust. Mechanical sawing avoids the HAZ but introduces burrs of 0.15–0.3 mm that must be hand-deburred before orbital welding, and the clamping force required to hold a 6 m tube against a cold saw blade routinely ovalizes the section by 0.2–0.5 mm — enough to compromise a 37° JIC flare seat.
Fiber laser cutting at 1.07 µm wavelength sidesteps both failure modes. The kerf is 0.15–0.25 mm depending on nozzle selection, the HAZ is typically under 0.08 mm with nitrogen assist, and there is no mechanical contact force beyond chuck clamping.
| Parameter | Plasma Cutting | Mechanical Sawing | Fiber Laser (1.07 µm) |
|---|---|---|---|
| Kerf width | 1.2–2.0 mm | 2.5–4.0 mm (blade) | 0.15–0.25 mm |
| HAZ depth on SUS304 | 0.4–0.9 mm | None (mechanical) | <0.08 mm (N₂ assist) |
| Burr height | 0.10–0.25 mm dross | 0.15–0.30 mm | <0.03 mm |
| Ovality induced on 6 m tube | 0.15–0.35 mm | 0.20–0.50 mm | <0.05 mm |
| Cut speed (2.0 mm wall) | 1.8–2.5 m/min | 0.3–0.6 m/min | 4.5–6.0 m/min |
| Post-process deburring | Required | Required | Eliminated |
| Consumable cost per meter | Electrode + nozzle | Blade + coolant | Nozzle + N₂ only |
Thermal Expansion Mitigation: The Real Constraint
A 6-meter SUS304 tube at 20°C ambient grows 1.04 mm when its mean temperature rises 10°C. In a depot where summer floor temperature swings from 18°C at 06:00 to 34°C by 14:00, that is a 2.8 mm positional drift across a shift if the tube is rigidly clamped at both ends. The laser head does not care about the tube’s absolute position — it cares about the relative position between the nozzle and the cut surface. Drift of 2.8 mm against a 0.2 mm kerf is a scrapped part.
The mitigation strategy is a floating front chuck with pneumatic pressure regulated to 0.4–0.6 MPa, not the 0.9–1.2 MPa used on thick-wall carbon pipe. Lower clamping pressure allows the tube to slide axially inside the jaw serrations as it expands, while a rear chuck holds 0.7–0.8 MPa to maintain feed authority. The differential is deliberate: the front chuck acts as a thermal slip joint, the rear chuck as the kinematic reference.
Bed stability follows the same logic. Cast-iron beds with bolted linear rails move 0.02–0.04 mm per °C of rail temperature rise. Stress-relieved welded steel beds with epoxy-granite infill hold under 0.008 mm/°C. For hydraulic line work where a 6 m tube may be cut in 40–60 seconds of arc time but sit clamped for 4 minutes of handling, the bed’s thermal time constant matters more than its static stiffness.
Process Parameters That Hold Tolerance
- Laser source: 3–6 kW single-mode fiber, 1.07 µm, duty cycle 60–80% for continuous tube feed
- Assist gas: Nitrogen 99.999%, delivery pressure 1.2–1.5 MPa at the nozzle, 12–18 bar regulated
- Oxygen only for sacrificial pierce on 3.0 mm wall, then switch to N₂ for the contour
- Focus position: -0.5 to -1.0 mm below surface for 2.0 mm SUS304
- Cut speed: 4.5–6.0 m/min at 2.0 mm wall, 3.2–4.0 m/min at 3.0 mm
- Chuck pneumatic pressure: front 0.4–0.6 MPa, rear 0.7–0.8 MPa
- Nozzle standoff: 0.8–1.2 mm, single orifice 1.5 mm for N₂ cutting
Pierce time on 3.0 mm SUS304 with N₂ runs 0.6–0.9 seconds. Multiply that by 40 pierce events per tube and you have 24–36 seconds of pure thermal loading before a single contour is cut. This is why duty cycle management and inter-pierce dwell logic in the CNC are not optional features — they are the difference between a 0.05 mm ovality and a 0.20 mm ovality after 200 tubes.
Field Verification Protocol
Post-cut inspection on locomotive hydraulic lines should include laser micrometer ovality scan at three stations (0°, 90°, 180°), flare seat angle verification to ±0.5°, and dye-penetrant check on the HAZ boundary. A properly tuned cell running SUS304 at the parameters above will hold ovality under 0.05 mm and flare seat concentricity within 0.08 mm TIR across a full shift, provided the bed is stress-relieved and the front chuck pressure is not cranked up “for safety.”
FAQ: Procurement and Specification Questions
What laser power is required for cutting 3.0 mm SUS304 locomotive hydraulic tube?
A 3 kW single-mode fiber source is the practical minimum for 3.0 mm wall at production speeds of 3.2–4.0 m/min with nitrogen assist. A 6 kW source allows higher duty cycle and faster pierce on thicker sections, but for 12–25 mm OD hydraulic line work, 3–4 kW is the sweet spot for kerf quality and gas consumption.
Why is nitrogen preferred over oxygen for stainless tube laser cutting?
Oxygen assist produces an exothermic reaction that accelerates cutting but leaves an oxidized kerf edge with chromium depletion, which becomes a corrosion initiation site in hydraulic service. Nitrogen at 1.2–1.5 MPa produces a clean, oxide-free kerf with HAZ under 0.08 mm, preserving the alloy’s corrosion resistance at the weld collar.
How does chuck clamping pressure affect tube ovality on long hydraulic lines?
Excessive front chuck pressure above 0.8 MPa ovalizes thin-wall SUS304 and prevents axial thermal slip, causing positional drift of up to 2.8 mm over a shift. Regulating front chuck to 0.4–0.6 MPa and rear chuck to 0.7–0.8 MPa allows thermal expansion to slide through the front jaw while maintaining feed authority, holding ovality under 0.05 mm.













