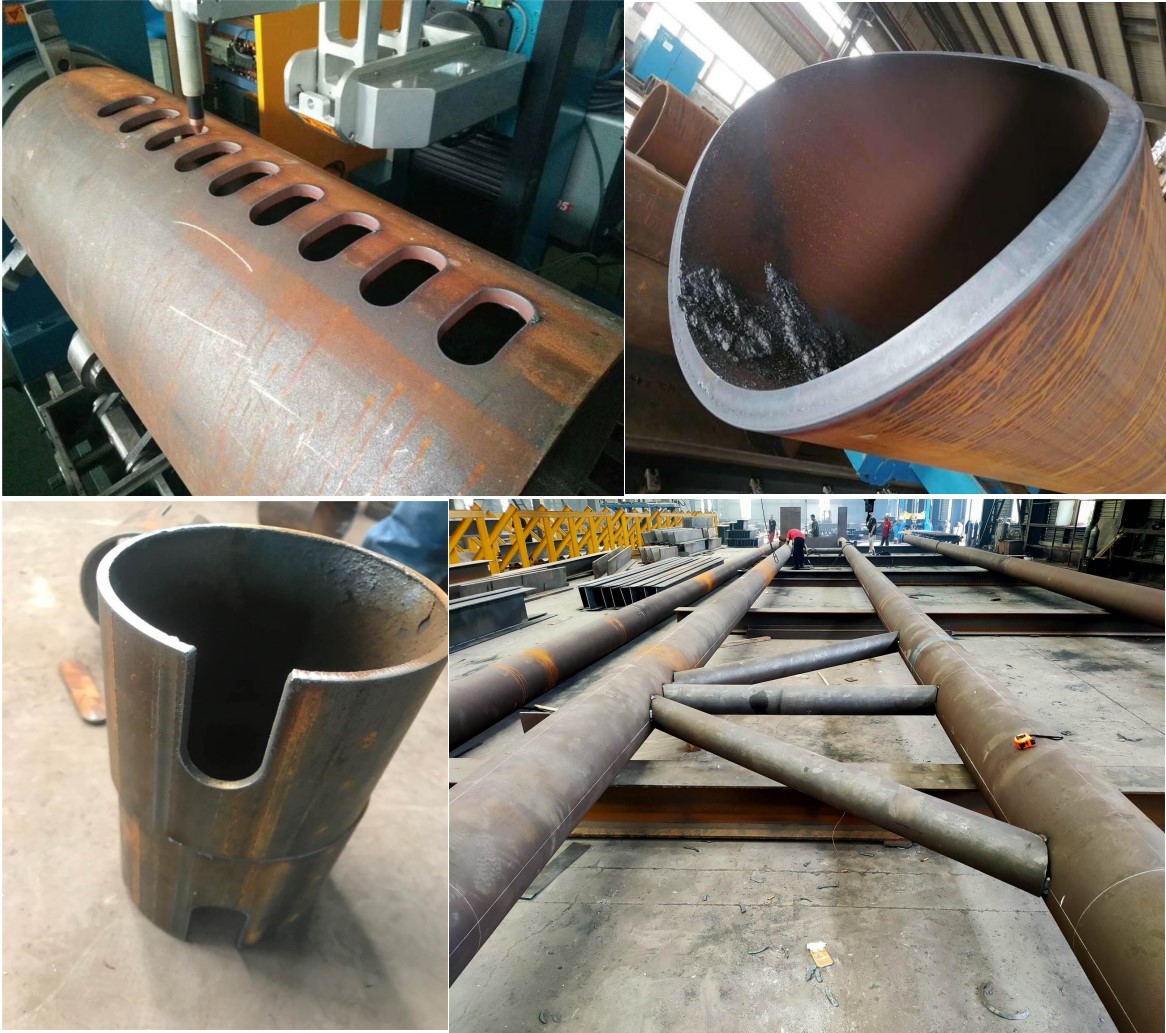
Shop-Floor Realities of Tube Laser Integration for Ergonomic Office Chair Frame Production
The ergonomic office chair frame is a deceptively hostile assembly from a fabrication standpoint. A single mid-back task chair typically carries 42 to 68 discrete tube nodes — armrest supports, seat pan perimeter loops, gas-lift cradles, lumbar cross-members, and five-star base legs — each with compound miter cuts, slot features, and weld-prep edge geometry. When a shop transitions from manual sawing and plasma profiling to an automatic fiber laser tube cutter for ergonomic office chair frames, the engineering conversation shifts from “can we cut it” to “can we hold tolerance across a 4,000-piece monthly mix while keeping the chuck jaws from crushing 1.5 mm wall stock.” That is the real problem statement.
Workflow Architecture: From Coil to Welded Sub-Assembly
A functional tube laser cell for chair frame work is not a standalone machine — it is a node inside a material flow. The typical layout I commission runs as follows:
- Raw stock staging: 6-meter bundles of S355JR (EN 10025-2) and SUS304 tube, OD range 19 mm to 42 mm, wall thickness 1.2 mm to 2.5 mm. Al6061-T6 is reserved for premium armrest spines where weight targets drop below 380 g per side.
- Infeed loading: Bundle loader with V-groove chain transfer, 500 kg capacity, cycle time 38 seconds per 6 m bar.
- Chuck clamping: Dual pneumatic self-centering chucks, front chuck 0.6–0.8 MPa, rear chuck 0.4–0.5 MPa. Wall thickness below 1.5 mm demands pressure reduction to 0.35 MPa with soft urethane jaw inserts to prevent ovalization beyond 0.08 mm.
- Cutting head: 3 kW single-mode fiber source, 1,080 nm wavelength, collimation 100 mm, focus 125 mm, spot diameter 0.08 mm at focus.
- Outfeed and sorting: Servo-driven catch tray with part-specific chutes, segregated by weldment family to feed the robotic MIG cell directly.
Material Tolerance and Laser Absorption Efficiency
Absorption behavior is wavelength- and surface-dependent. At 1,080 nm, cold-rolled S355JR with a mill finish reflects roughly 62–68% of incident energy at room temperature; once the melt pool forms and surface temperature exceeds 1,500 °C, absorptivity climbs to 80–85%. This is why pierce parameters matter more than cut parameters on thin-wall chair tubing. A 2.5 mm S355JR pierce runs at 1,200 W peak, 30% duty cycle, 200 Hz modulation, 0.3 s dwell — anything hotter and you blow a keyhole through the far wall.
SUS304 behaves differently. Reflectivity at 1,080 nm sits near 70% cold, but thermal conductivity (16.2 W/m·K) is roughly one-third that of carbon steel, so heat concentrates. Nitrogen assist at 1.4–1.5 MPa, 99.999% purity, produces the oxide-free edge required for downstream robotic MIG without acid pickling. Cutting speed on 1.5 mm SUS304 at 3 kW lands around 6.8 m/min with a 0.8 mm nozzle at 1.2 mm standoff.
Al6061-T6 introduces the worst case. Reflectivity exceeds 85% at 1,080 nm, and the alloy’s high thermal diffusivity (167 W/m·K) wicks heat away from the kerf. Nitrogen at 1.5 MPa with a 1.2 mm nozzle and 0.5 mm standoff is mandatory; oxygen assist is prohibited because it produces an Al₂O₃ dross layer that destroys weld integrity on the armrest spine joints.
Dimensional tolerance on chair frames is governed by two stacked error sources: chuck runout (target ≤ 0.05 mm TIR) and thermal drift in the cutting head over a 6-hour shift. On a properly aligned machine running 22 °C ambient, I hold ±0.10 mm on hole position and ±0.15° on miter angle across a full bar. That is the envelope the weld fixture expects.
Comparative Process Data: Legacy vs. Fiber Laser Tube Cutting
| Parameter | Mechanical Saw + Drill | Plasma Tube Profiling | Fiber Laser Tube Cutter (3 kW) |
|---|---|---|---|
| Cut tolerance (mm) | ±0.5 | ±0.8 | ±0.10 |
| Miter angle accuracy | ±1.5° | ±1.0° | ±0.15° |
| Heat-affected zone | None (cold) | 0.8–1.5 mm | 0.05–0.15 mm |
| Edge prep for MIG | Deburr + chamfer op | Grind required | Weld-ready, oxide-free (N₂) |
| Cycle time per chair set (68 nodes) | ~42 min | ~18 min | ~6.5 min |
| Consumable cost per meter | Blade + drill bits | Electrode + nozzle + shield gas | Nozzle + N₂/O₂ only |
| Wall thickness limit (min) | 1.5 mm (crush risk) | 2.0 mm | 0.8 mm |
| Nesting / scrap rate | 8–12% | 5–7% | 1.5–2.5% |
Gas Delivery and Duty Cycle Discipline
Nitrogen delivery at the nozzle must be regulated at 1.2 to 1.5 MPa with a flow rate of 18–25 L/min for thin-wall stainless. Below 1.2 MPa, dross adhesion on the bottom kerf edge becomes measurable, and the downstream weld cell sees porosity. Oxygen assist for S355JR runs at 0.6–0.9 MPa with a slightly larger nozzle (1.2 mm) to stabilize the exothermic reaction on 2.5 mm wall stock.
Duty cycle discipline is where shops lose money. A 3 kW source running 68-node chair sets at 70% duty over an 8-hour shift accumulates thermal load in the resonator and cutting head optics. I mandate a 12-minute cooldown window every 90 minutes, or active water chilling at 22 °C ± 1 °C on the head. Skipping this drifts focus position by 0.3 mm over four hours — enough to fail a miter tolerance check on the armrest spine.
Procurement FAQ
What tube diameter and wall thickness range should a chair frame laser cutter support?
Specify a machine with a 20 mm to 120 mm OD capacity and a minimum wall handling of 0.8 mm. Chair frames rarely exceed 42 mm OD, but the 0.8 mm floor is critical for Al6061 armrest spines and thin-wall SUS304 lumbar loops. Verify chuck pressure control down to 0.3 MPa to avoid tube ovalization.
Is nitrogen assist mandatory for stainless chair frame tubes?
Yes for SUS304 and Al6061. Nitrogen at 1.4–1.5 MPa, 99.999% purity, delivers oxide-free edges that accept robotic MIG without pickling. Oxygen assist is acceptable only on S355JR carbon steel where the weld cell performs a post-weld grind.
What tolerance should I contractually require from the tube laser supplier?
Demand ±0.10 mm on hole position, ±0.15° on miter angle, and ≤ 0.05 mm chuck runout (TIR) verified with a dial indicator at the front chuck face. Any supplier quoting looser tolerances will transfer rework cost to your weld fixture and inflate your scrap rate above 4%.













