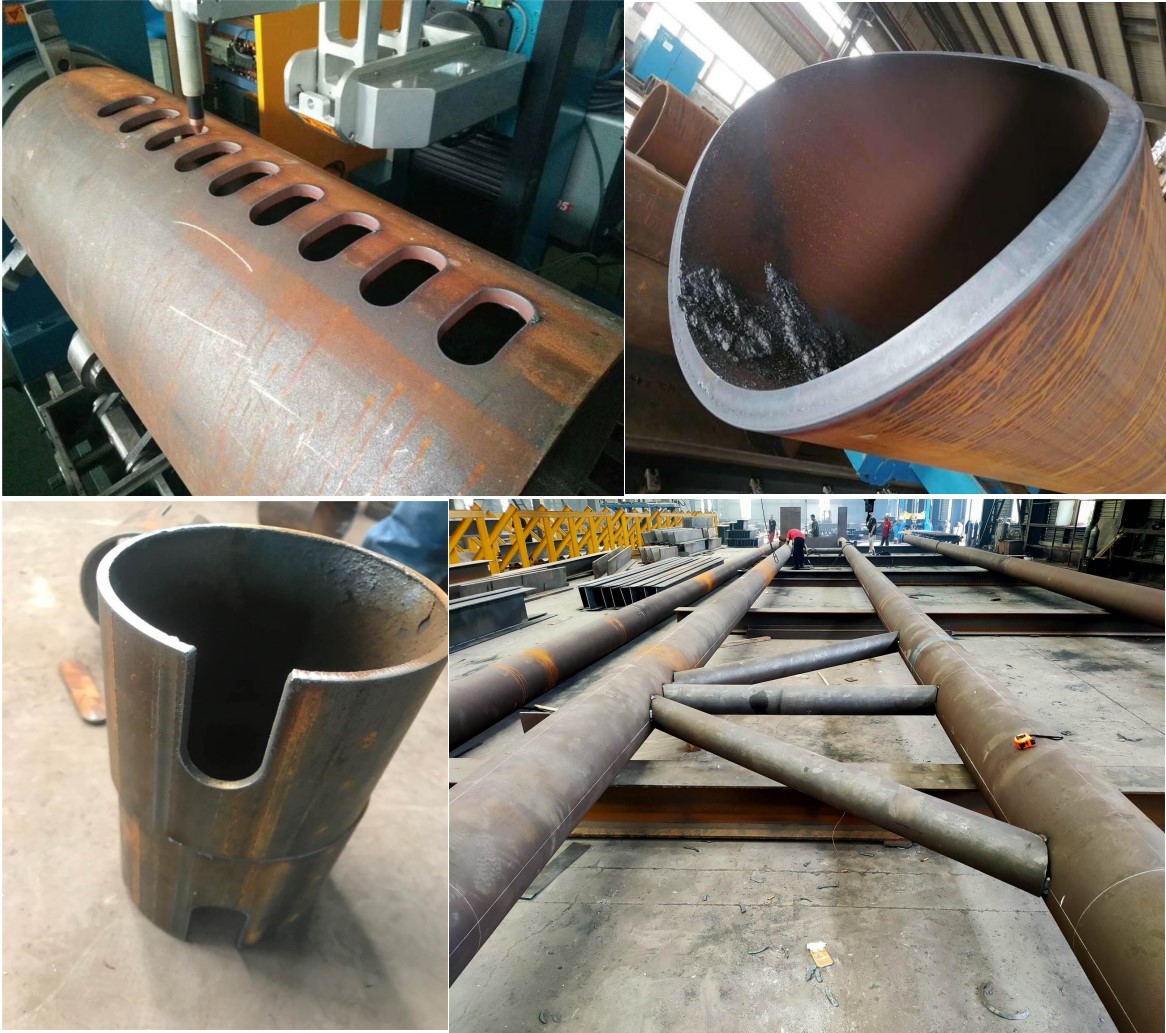
Advanced Nesting Algorithms and Common-Line Cutting Strategy in Automated Tube Laser Production Lines for Power Grid Pylons
When you are cutting 12-meter Q345B or S355JR angle steel for a 500kV transmission tower, the difference between a 68% and an 82% material yield rate is not a purchasing decision — it is a physics problem. Most fabrication shops running an automated tube laser production line for power grid pylons still operate their nesting software on default parameters inherited from flat-sheet cutting, which is fundamentally wrong for tubular profiles. The cutting head on a 6kW fiber source traverses a rotating 3D contour, not a 2D plane, and the kerf compensation logic must account for chordal deviation on the tube’s outer diameter. Ignoring this costs roughly 4 to 7% additional scrap per shift on high-volume pylon contracts.
Why Pylon Tube Geometry Breaks Conventional Nesting Logic
Power grid pylon members are not simple round tubes. The dominant profiles are L-angle (50×50×5 to 200×200×16), channel, and occasionally square hollow sections in SUS304 for coastal corrosion zones. Each cross-section introduces a unique nesting constraint:
- Angle steel has an asymmetric mass distribution. When the chuck rotates at 60 rpm during a contour cut, the inertial moment shifts, and the pneumatic chuck pressure must be regulated between 0.6 and 0.8 MPa to prevent slippage without crushing the leg.
- Square tube (SHS) requires corner-radius-aware lead-in placement. A standard 0.5mm lead-in on a flat sheet becomes a 1.2mm effective pierce on a 90° corner, causing dross adhesion.
- Round tube for bracing members (typically Ø60×3 to Ø168×6, SUS304 or Al6061) demands rotational synchronization within ±0.05° to avoid taper on the cut face.
The nesting engine must therefore treat each profile as a parametric solid, not a flattened development. Modern CAM suites (SigmaNEST, Lantek Flex3d, or the proprietary nesting module bundled with high-end tube lasers) apply a 3D collision envelope that accounts for the chuck jaw geometry, the nozzle standoff (typically 0.8–1.2mm for oxygen cutting, 1.5–2.0mm for nitrogen), and the focal position drift across the tube’s curvature.
Common-Line Cutting Strategy: The Yield Multiplier
Common-line cutting — where two adjacent parts share a single kerf — is the single highest-leverage yield strategy on pylon tube lines. On a 12m S355JR angle, a well-configured common-line nest can recover 180 to 240mm of material per bar compared to a gap-nested layout. The mechanics are straightforward: instead of two separate pierces and two kerfs (each 0.15–0.25mm wide on a 1.5kW–6kW fiber source), you execute one pierce and one shared cut.
The catch is thermal. When you common-line cut S355JR at 4kW with oxygen assist at 1.2 MPa, the heat-affected zone (HAZ) on the shared edge can reach 0.3–0.5mm. If the downstream process is galvanizing (standard for pylon members per ASTM A123), that HAZ is acceptable. If the member is going into a bolted joint with tight tolerance (±0.5mm), the shared edge must be re-machined or the common-line strategy abandoned for that specific joint.
Practical parameters observed on a 6kW IPG source cutting 8mm S355JR angle:
- Cutting speed: 2.8–3.2 m/min
- Laser power: 4.5–5.0 kW (duty cycle 85%)
- Frequency: 1,200–1,500 Hz (modulated for edge quality)
- Oxygen pressure: 1.2–1.4 MPa
- Focal position: -1.5mm (below surface)
- Kerf width: 0.20–0.25mm
Nitrogen cutting on SUS304 at 6mm thickness runs at 1.5 MPa, 3.5 m/min, with a 0.15mm kerf — but the gas consumption cost is roughly 3.2× that of oxygen cutting. For pylon work where 70% of the tonnage is carbon steel, oxygen remains the economic default.
Comparative Technical Data: Legacy vs. Fiber Laser Tube Processing
| Parameter | Conventional Plasma / Mechanical Saw | Fiber Laser Tube Line (6kW) |
|---|---|---|
| Cut tolerance (mm) | ±1.5 (plasma), ±2.0 (saw) | ±0.10 to ±0.15 |
| Kerf width (mm) | 3.0–5.0 (plasma), 4.0 (saw blade) | 0.15–0.25 |
| HAZ depth (mm) | 1.5–3.0 | 0.2–0.5 |
| Nesting yield on 12m S355JR angle | 62–68% | 78–84% (with common-line) |
| Pierce time per hole (s) | N/A (drill) 4–8s | 0.3–0.8 |
| Setup changeover (min) | 15–25 | 2–4 (auto chuck + program recall) |
| Consumable cost per meter | $0.45–$0.80 (electrode/nozzle/blade) | $0.12–$0.22 (nozzle + lens amortized) |
| Edge finish (Ra µm) | 12.5–25 | 3.2–6.3 |
Material Yield Maximization: The Software Layer
Yield on a pylon tube line is a function of three stacked variables: bar length utilization, remnant management, and dynamic re-nesting. Bar length utilization is the obvious one — a 12m bar cut into 11.7m of parts leaves 300mm of remnant. Over 500 bars, that is 150 meters of scrap. The nesting engine must be able to accept a “remnant priority” flag that pulls from the remnant rack before consuming a new bar.
Dynamic re-nesting is where the real yield gain lives. When a pylon contract specifies 47 different member lengths across 3 profiles, a static nest wastes 6–9% on average. A dynamic engine that re-optimizes the cut sequence every 10 bars, accounting for actual remnant lengths and current order backlog, recovers 3–5% of that. On a 2,000-ton pylon project, that is 60–100 tons of steel — at $750/ton for S355JR, a $45,000–$75,000 swing.
The software must also handle the “cut-then-mark” vs. “mark-then-cut” decision. For pylon members requiring traceability stamps (heat number, member ID), the laser can mark at 30% power with a defocused beam, adding 0.4–0.6s per mark. If the mark is placed in the nesting layout as a shared operation across two parts, the time cost drops by half.
Integration with Downstream Pylon Fabrication
The tube laser does not exist in isolation. On a pylon line, it feeds directly into a robotic drilling station (for bolt holes beyond laser range), a bending press, and a welding cell. The nesting software must output not just the cut program but also a sequence file that matches the downstream station’s takt time. If the laser cuts 40 members per hour but the welding cell consumes 32, you have a 25% buffer accumulation — which is fine for a 2-shift operation but becomes a bottleneck on a 3-shift sprint.
The practical fix is to nest by downstream grouping: all members for one pylon section cut in sequence, so the buffer is section-complete rather than member-complete. This reduces WIP inventory by 30–40% and simplifies the kitting operation.
Frequently Asked Questions
What is the typical material yield improvement when switching from plasma to fiber laser on pylon tube production?
On 12m S355JR angle steel, the yield improvement is typically 12 to 18 percentage points, driven primarily by reduced kerf width (0.20mm vs. 3.5mm) and the ability to apply common-line cutting. A shop running 2,000 tons per year can expect to recover 240–360 tons of additional usable material, translating to $180,000–$270,000 in annual steel cost savings at current S355JR pricing.
Can a fiber laser tube line cut SUS304 and Al6061 on the same machine without contamination issues?
Yes, but with strict changeover protocol. SUS304 requires nitrogen assist at 1.5 MPa to prevent oxidation, while Al6061 cuts best with nitrogen at 1.2–1.4 MPa and a higher focal position. The critical issue is cross-contamination: stainless steel dust on aluminum can cause galvanic corrosion. The line must include a dedicated extraction and a purge cycle of 30–45 seconds between material changes, plus separate nozzle inventories.
What chuck pneumatic pressure is required for high-speed rotation on asymmetric profiles like angle steel?
For L-angle profiles from 50×50×5 to 200×200×16, the chuck pressure should be regulated between 0.6 and 0.8 MPa. Below 0.6 MPa, slippage occurs at rotation speeds above 45 rpm. Above 0.8 MPa, the chuck jaws can deform the angle’s leg, causing dimensional deviation of 0.3–0.5mm. Modern lines use a closed-loop pressure regulator that adjusts dynamically based on the rotational speed profile of the cut program.













