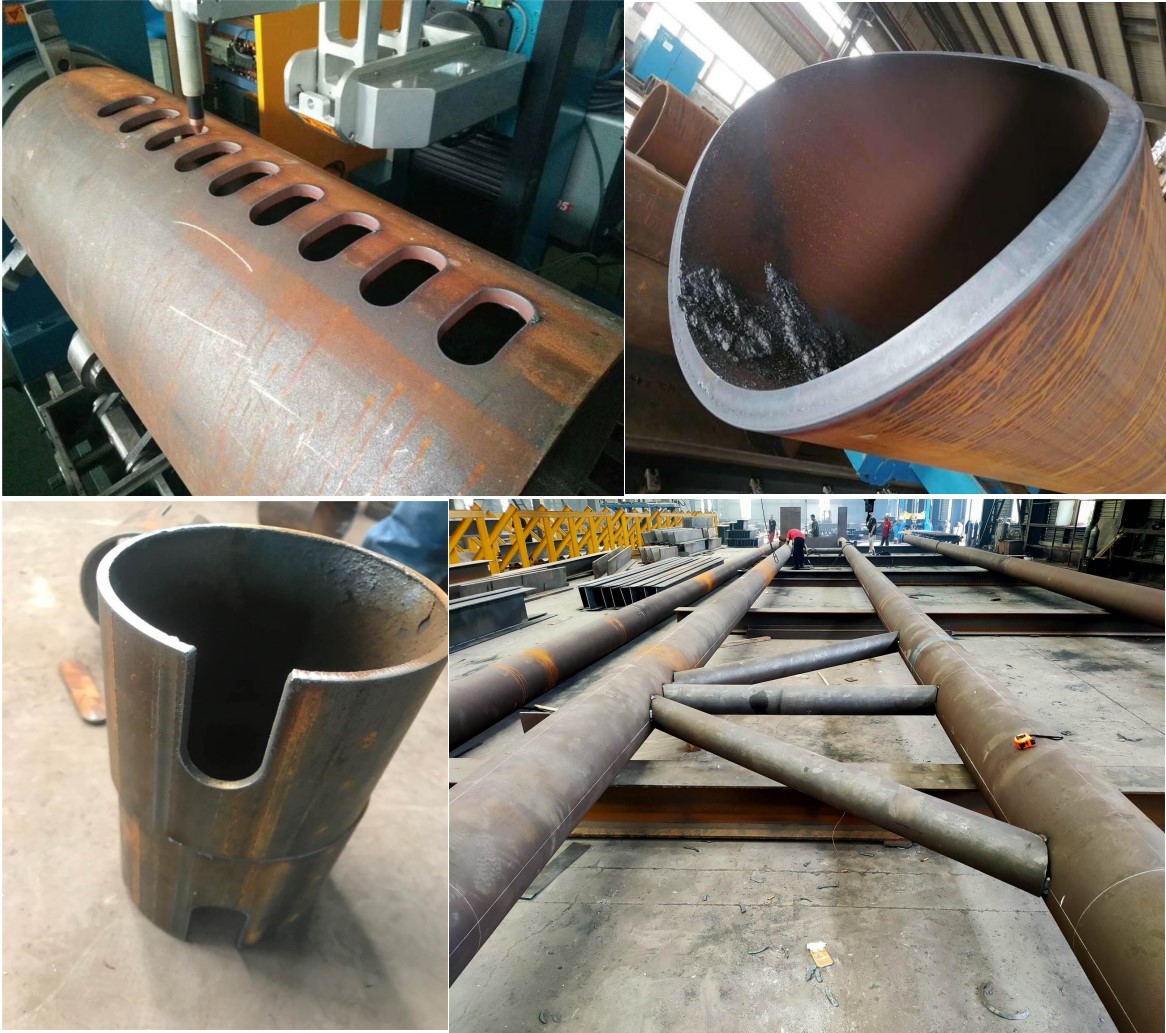
Automatic Chuck Tube Laser Integration for Heavy-Duty Building Column Fabrication: Automation Interfacing, Bundling Loaders, and MES/ERP Data Architecture
Structural steel fabricators running 12-meter W-beams, S355JR box columns, and SUS304 architectural tubes face a throughput ceiling that has nothing to do with the laser source itself. The bottleneck sits at the material handling interface: manual crane loading, operator-dependent chuck jaw positioning, and disconnected production data. For shops evaluating an automatic chuck tube laser for heavy duty building column fabricators, the real engineering decision is not wattage — it is how the machine talks to the bundling loader upstream and the MES/ERP stack downstream.
Why Heavy Column Work Breaks Conventional Cutting Methods
Building column profiles — typically 200×200 to 400×400 mm square tube, 12 mm to 25 mm wall thickness in S355JR, or 300 mm diameter pipe in SUS304 — carry mass that punishes every non-laser process. A 12-meter S355JR box section at 20 mm wall weighs roughly 1.4 tonnes. Plasma cutting at 200 A on 20 mm S355JR produces a heat-affected zone of 1.5–3.0 mm, requires secondary grinding, and cannot hold the ±0.5 mm hole-to-hole tolerance demanded by bolted end-plate connections. Mechanical sawing is dimensionally acceptable but offers zero profile capability — no copes, no bolt slots, no weld-prep bevels in a single pass.
Fiber laser cutting on these sections, delivered through a 6 kW to 12 kW source at 1,060–1,080 nm wavelength, changes the thermal equation. Cutting 20 mm S355JR with nitrogen at 1.4 MPa delivery pressure and a 1.2 mm nozzle orifice yields a kerf of approximately 0.8 mm with a roughness Ra under 6.3 µm — no secondary operation. For SUS304 at 12 mm, high-pressure N2 at 1.5 MPa with a 200 Hz pulse frequency on the piercing cycle prevents dross adhesion on the bottom edge. Duty cycle matters: continuous 100% duty at 8 kW on 15 mm mild steel draws roughly 28–32 kW from the wall, and the chiller loop must dissipate 18–22 kW of thermal load. Undersized facility cooling is the single most common commissioning failure on these installations.
Chuck Architecture and Pneumatic Clamping Physics
An automatic chuck on a heavy column machine is not a scaled-up tube chuck. It is a synchronized four-jaw or six-jaw system with independent servo positioning on the X and Y axes. Jaw travel of 20–500 mm accommodates the profile range without manual intervention. Clamping force is generated pneumatically, typically 0.6–0.8 MPa shop air feeding a booster circuit that multiplies to 3.5–5.0 MPa at the jaw cylinder — sufficient to resist the torsional moment induced when the cutting head accelerates along a 12-meter axis at 80 m/min traverse.
The critical parameter is jaw pressure compensation. On a 400×400 mm S355JR column, wall thickness variation of ±0.8 mm across the section means a fixed clamping pressure will either crush thin-wall zones or allow micro-slip on thick zones. Modern automatic chucks use proportional pressure regulators tied to the CNC, adjusting clamp force per profile recipe. Slip of even 0.3 mm during a 6-meter cut destroys positional accuracy on downstream bolt holes.
Upstream Automation: Auto-Bundling Loader Interfacing
The loader is where most integration projects fail. A heavy-duty column shop receives material in bundles of 5–10 pieces, banded, often with surface rust and mill scale. The auto-bundling loader must:
- De-band and singulate without scratching SUS304 or Al6061 surfaces (Al6061 requires urethane-lined V-rollers; steel-on-steel contact causes galling)
- Measure each tube’s actual length and cross-section via laser profilometer, feeding corrected offsets to the chuck CNC before clamping
- Transfer to the chuck infeed zone with positional repeatability under ±1.0 mm — anything looser forces the chuck to re-home, adding 8–14 seconds per cycle
- Handle mixed-profile bundles when the ERP work order sequences different column sizes back-to-back
The handshake protocol between loader PLC and laser CNC is typically Profinet or EtherCAT at 100 Mbit/s, with a dedicated safety PLC on a separate FSoE channel. Cycle time budget for a 12-meter S355JR column with 40 piercings and 18 meters of cut length: load 45 s, clamp and datum 12 s, cut 6–9 min depending on thickness, unload 35 s. The loader must be ready to receive the finished part before the cut completes — pre-positioning logic, not sequential logic.
Downstream and MES/ERP Integration Layer
Post-cut, the part moves to an unloading station or directly to a welding fit-up bay. The MES integration is where traceability is won or lost. Each column carries a work order ID from the ERP (SAP, Epicor, or similar). The laser CNC writes back:
- Actual cut length and pierce count per part
- Nesting efficiency and remnant length returned to stock
- Machine utilization, gas consumption (Nm³ of N2 per part), and power draw
- Any deviation flags — kerf width drift, pierce failures, chuck re-clamp events
This data flows via OPC UA or MTConnect to the MES, which reconciles against the ERP bill of materials. A shop cutting 200 tonnes of S355JR monthly typically recovers 3–5% material yield through remnant tracking alone — on 200 tonnes at €850/tonne, that is €5,100–€8,500 monthly. The integration pays for itself before the laser’s depreciation schedule reaches year two.
Comparative Technical Data: Conventional vs. Automatic Chuck Laser
| Parameter | Plasma / Mechanical Saw (Conventional) | Automatic Chuck Tube Laser |
|---|---|---|
| Dimensional tolerance (hole position) | ±1.5–2.5 mm (plasma), ±0.5 mm (saw, straight cuts only) | ±0.1–0.3 mm |
| Heat-affected zone (20 mm S355JR) | 1.5–3.0 mm, requires grinding | <0.15 mm, no secondary op |
| Profile capability | Copes and slots require separate ops | Single-pass copes, slots, bevels |
| Cutting speed (20 mm mild steel) | Plasma ~1.8 m/min | Laser ~1.2–1.6 m/min (6 kW), 2.2–2.8 m/min (12 kW) |
| Consumable cost per meter | Plasma: electrodes, nozzles, shielding gas | N2 at 1.4 MPa, lens protection window |
| Labor per part (12 m column) | 2 operators, 3–4 hrs including rework | 0.5 operator, 35–50 min |
| MES/ERP data feedback | Manual entry, error-prone | Automated OPC UA / MTConnect |
| Material yield (remnant tracking) | Baseline | +3–5% recovery |
Commissioning Pitfalls Specific to Column Fabrication
Three failure modes recur across installations. First, foundation isolation — a 12-meter machine with a 1.4-tonne moving mass generates dynamic loads that crack inadequate concrete pads within 18 months; specify a minimum 300 mm reinforced pad with vibration isolators rated to the machine’s dynamic envelope. Second, gas delivery — nitrogen at 1.4–1.5 MPa requires a bulk tank with a properly sized evaporator; undersized evaporators cause pressure droop mid-cut, producing dross on the final 2 meters of a 12-meter column. Third, chuck jaw wear — on S355JR with mill scale, jaw inserts wear 0.2–0.3 mm per 1,000 parts; without a wear-compensation routine in the CNC, positional accuracy degrades silently.
FAQ: Industrial B2B Procurement
What laser power is required for 25 mm S355JR building columns?
A 12 kW fiber source is the practical minimum for 25 mm S355JR at production speeds with nitrogen assist. A 6 kW source will cut the thickness but at 0.6–0.8 m/min, which is uneconomical for 12-meter columns. For 20 mm and below, 8 kW delivers the best cost-per-meter balance.
How does the auto-bundling loader handle mixed-profile bundles from the ERP?
The loader reads the work order sequence from the MES via OPC UA, then uses a laser profilometer to verify each tube’s actual cross-section before transfer. If the measured profile deviates from the ERP entry by more than 2 mm, the loader diverts the tube to a quarantine station rather than risk a chuck mis-clamp.
What is the typical payback period for full MES/ERP integration on a heavy column laser cell?
For a shop processing 150–250 tonnes monthly, the combination of remnant recovery (3–5% yield), labor reduction (1.5 operators per shift), and elimination of secondary grinding typically yields payback in 14–22 months, assuming two-shift operation and 75% machine utilization.













