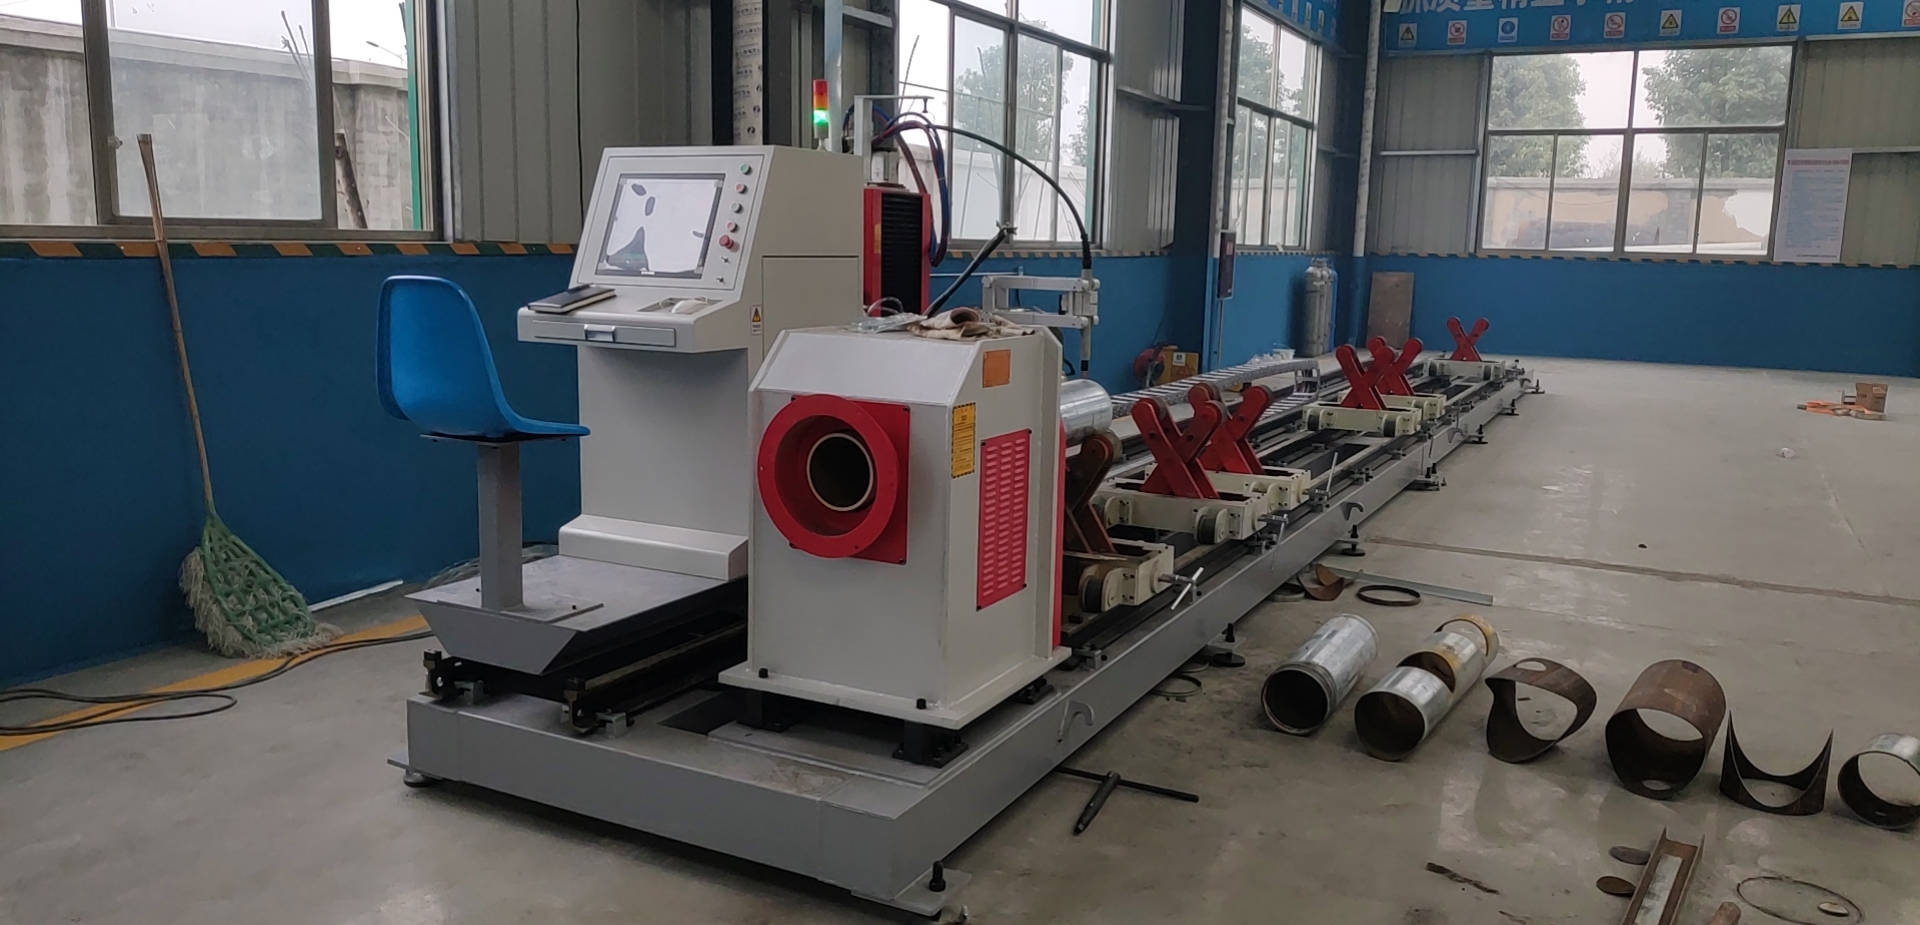
Material-Grade Metallurgy and the EN 1090 Compliance Trap in Axle Housing Fabrication
Heavy truck axle housings are not decorative tubular assemblies. They are Class 3 load-bearing structural members subjected to torsional fatigue cycles exceeding 10^7 reversals, dynamic bending moments from road input, and weld-induced residual stress fields that concentrate at the banjo-to-spindle transition zone. When a fleet operator in the EU specifies an axle housing, the fabrication route must satisfy EN 1090-2 Execution Class EXC 3 as a baseline, which drags the cutting process into a certification envelope most job shops underestimate. A fiber laser pipe cutting machine for heavy truck axle housing is not simply a throughput upgrade over plasma or band sawing — it is the process control instrument that determines whether your weld procedure qualification records (WPQR) survive third-party notified body review.
The dominant substrate is S355JR hot-rolled seamless tube (yield 355 MPa, tensile 470–630 MPa) with wall thickness ranging 8 mm to 16 mm at the spindle shoulder and up to 22 mm at the differential carrier flange. Some premium OEMs migrate to S460NH for weight reduction, which introduces a whole new heat-affected zone sensitivity problem. Cutting method selection directly governs the HAZ width, edge squareness, and oxide inclusion density that the subsequent MAG weld must tolerate.
Why Plasma and Sawing Fail the Certification Audit
Conventional plasma cutting on 16 mm S355JR produces a kerf taper of 3–6 degrees and a recast layer 0.05–0.12 mm thick with embedded nitrides. That recast layer is a crack initiation site under EN 1090-2 Clause 6.4 fatigue assessment. Mechanical band sawing avoids thermal damage but delivers ±0.5 mm length tolerance and requires secondary milling of weld prep bevels — a two-setup process that destroys datum continuity. When the notified body audits dimensional traceability under EN 1090-2 Annex B, the saw-plus-mill route generates a paper trail of re-clamping errors that is nearly impossible to defend.
Fiber laser cutting at 1.07 µm wavelength eliminates both problems. The focused spot at 0.15–0.25 mm with a Rayleigh length tuned for 12 mm S355JR produces a kerf width of 0.3–0.6 mm, perpendicularity within 0.05 mm over the full wall, and an HAZ of 0.08–0.15 mm with no recast adhesion when oxygen assist is correctly parameterized.
Comparative Process Data — Axle Housing Tube Cutting
| Parameter | Plasma Cutting | Mechanical Band Saw + Milling | Fiber Laser (3–6 kW, IPG/Raycus source) |
|---|---|---|---|
| Cut edge perpendicularity | 3–6° taper | 0.1 mm (after milling) | ≤0.05 mm |
| HAZ width on S355JR (12 mm) | 0.4–0.9 mm | None (mechanical) | 0.08–0.15 mm |
| Length tolerance (2 m tube) | ±0.8 mm | ±0.5 mm | ±0.05 mm |
| Cycle time per spindle cut | 45–70 s | 90–140 s (two setups) | 18–28 s |
| Assist gas | Air/N2, 0.6–0.9 MPa | None | O2 at 1.2–1.5 MPa (carbon steel) / N2 at 1.4–1.8 MPa (SUS304) |
| Post-cut operation | Grinding recast | Bevel milling | None |
| EN 1090-2 EXC 3 readiness | Conditional | Conditional | Compliant with documented PQR |
Chuck Dynamics and Pneumatic Clamping Reality
Axle housing tubes are rarely straight. Hot-rolled seamless stock carries ovality up to 1.2% and bow of 3 mm per meter. A four-jaw independent pneumatic chuck running at 0.6–0.8 MPa clamping pressure will distort a thin-wall section (8 mm) if jaw contact area is insufficient. The correct configuration is a dual-chuck arrangement — front chuck with 4 jaws at 0.7 MPa, rear chuck with 3 jaws at 0.5 MPa — plus a steady rest at mid-span to suppress whipping during 60–80 rpm rotation. Servo-driven chuck synchronization must hold angular phase error below 0.02 degrees or the cut seam at the banjo intersection drifts.
For SUS304 axle variants (rare but present in cryogenic and specialty transport), nitrogen assist at 1.4–1.8 MPa with a 4 kW source running 60% duty cycle produces dross-free edges. Al6061 housings for lightweight prototypes cut at 3 kW with N2 at 1.5 MPa and require focal position shifted +0.3 mm to avoid dross on the bottom kerf.
Global Compliance: EN 1090, ISO 3834, and the Traceability Chain
EN 1090-2 does not certify the machine — it certifies the factory production control (FPC) system. The laser cutter contributes three auditable outputs: cut length accuracy, edge quality class, and material traceability. A fiber laser with integrated nesting software that logs every cut parameter against the heat number of the incoming tube creates a digital thread that satisfies ISO 3834-2 Clause 6.7. Without that log, the fabricator is relying on manual records, which fail under notified body scrutiny.
For North American export, the same machine must satisfy AWS D1.1 Clause 5 for tubular connections and, for the axle specifically, FMVSS 223 rear impact guard adjacency requirements if the housing mounts to the frame rail. The cut face quality class per ISO 9013 must be documented as Class 3 or better (perpendicularity tolerance u ≤ 0.4 mm at 12 mm thickness) to avoid mandatory post-cut machining.
Procurement FAQ
What laser power is required to cut 16 mm S355JR axle housing tube without dross?
A 4 kW fiber source with oxygen assist at 1.3–1.5 MPa and a 1.2 mm nozzle at 0.8 mm standoff will cut 16 mm S355JR at 1.8–2.2 m/min with dross-free bottom edge. For 22 mm carrier flange sections, step to 6 kW with nitrogen at 1.6 MPa to maintain ISO 9013 Class 3 perpendicularity.
Can a fiber laser tube cutter maintain EN 1090-2 EXC 3 traceability automatically?
Yes, provided the CNC controller logs cut parameters (power, frequency, gas pressure, focal position, feed rate) against the tube heat number and exports the record in a format compatible with the FPC documentation package. This satisfies ISO 3834-2 Clause 6.7 and EN 1090-2 Annex B traceability requirements.
What chuck clamping pressure avoids ovality distortion on 8 mm wall axle tubes?
Limit front chuck clamping to 0.6–0.7 MPa with four-jaw contact and rear chuck to 0.5 MPa with three-jaw contact. Add a mid-span steady rest. Above 0.9 MPa on 8 mm S355JR, ovality deformation exceeds 0.3 mm and compromises the banjo weld fit-up.













