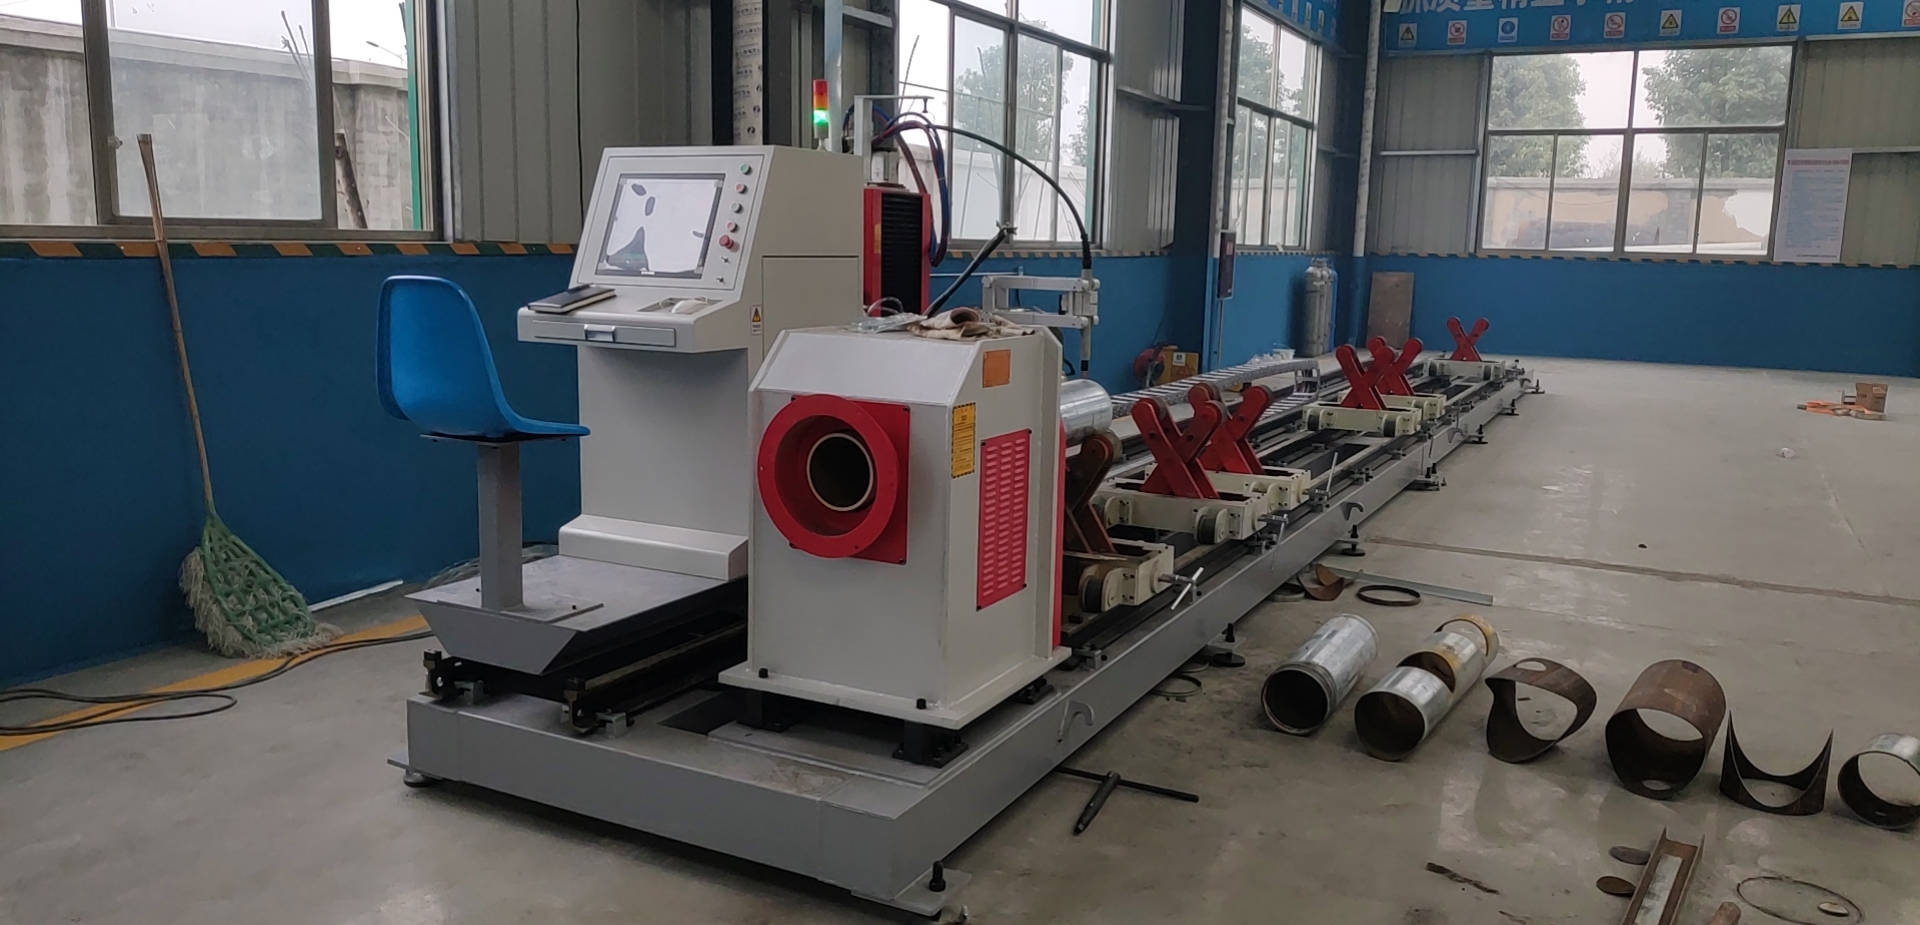
Maximizing Material Yield in Industrial Racking Tube Laser Cutting: Efficiency, Speed, and Beveling Dynamics
Industrial racking fabrication lives or dies on the arithmetic of scrap. When you are cutting S355JR square tube at 12 meters per minute, a 1.5% material loss on a 40,000-ton annual throughput translates into six figures of wasted steel. The shift from conventional plasma and mechanical sawing to fiber laser tube processing is not a cosmetic upgrade—it is a fundamental recalibration of how nested geometry, thermal input, and structural tolerances interact. For operations serious about maximizing material yield in industrial racking tube laser cutting, the gains come from three interlocking variables: processing efficiency, dynamic speed benchmarks, and the metallurgical control of structural beveling and root gap tolerances.
Processing Efficiency: Nesting Physics and Kerf Economics
The first yield lever is kerf width. A CO2 or plasma source on 3.0 mm wall S355JR typically produces a kerf of 0.8–1.2 mm. A 3 kW single-mode fiber laser running 1.2 mm nozzle standoff at 1.2 MPa nitrogen assist gas delivers a kerf of 0.15–0.25 mm. On a racking upright with 40+ bolt slots per tube length, that difference compounds. Across a 6-meter tube, kerf reduction alone recovers 18–30 mm of usable stock per part—enough to add one additional slot in many nesting scenarios.
Nesting strategy matters equally. Modern tube laser CAM software rotates the cutting head around the tube axis, allowing slot patterns to be interleaved across adjacent faces. On a 100x100x4 mm S355JR upright, this interleaving reduces the inter-part gap from 8 mm (plasma) to 2.5 mm (laser). The result is a yield improvement of 4–7% per tube, before any speed consideration.
Chuck and Clamping Dynamics
Yield is also lost to end-trim and clamping waste. Pneumatic chuck pressure must be tuned to the alloy. For SUS304 tube, 0.6–0.8 MPa clamping pressure prevents ovalization while maintaining grip. For Al6061-T6, pressure drops to 0.4–0.5 MPa to avoid surface marring and micro-cracking at the jaw contact. Setting these parameters correctly allows the operator to reduce the sacrificial end-trim from 150 mm to 80 mm, recovering 70 mm per tube—a 1.2% yield gain on a 6-meter length.
Dynamic Speed Benchmarks: Where the Real Yield Lives
Speed is not just throughput—it is thermal control. Excessive dwell time on thin-wall tube causes dross adhesion and heat-affected zone (HAZ) growth, which forces secondary grinding and increases scrap. The following table compares conventional methods against a 4 kW fiber laser tube system on 3.0 mm S355JR racking uprights.
| Parameter | Plasma Cutting | Mechanical Sawing | 4 kW Fiber Laser Tube |
|---|---|---|---|
| Cut speed (3 mm S355JR) | 2.8–3.5 m/min | 0.4–0.6 m/min | 10–14 m/min |
| Kerf width | 0.9–1.2 mm | 2.5–4.0 mm | 0.15–0.25 mm |
| HAZ width | 0.8–1.5 mm | 0.2–0.4 mm | 0.05–0.12 mm |
| Dross / post-processing | Heavy, requires grinding | Burr, requires deburring | Minimal, often none |
| Slot tolerance | ±0.5 mm | ±0.3 mm | ±0.05 mm |
| Nest gap (min) | 8 mm | N/A (single cut) | 2.5 mm |
| Yield loss per tube | 6–9% | 3–5% | 1.2–2.5% |
The speed differential is not linear with power. A 4 kW source at 1.3 MPa nitrogen cuts 3 mm S355JR at 12 m/min, but pushing to 6 kW only yields 15 m/min—a 25% speed gain for 50% more power. The yield-optimal configuration is often a 3–4 kW source with a 50 µm delivery fiber, which maintains beam quality (M² < 1.3) and keeps the kerf narrow. Duty cycle matters: at 80% duty cycle on a 4 kW head, the resonator holds stable output for 45-minute continuous runs, which is critical when cutting 200+ racking uprights per shift without thermal drift.
Structural Beveling and Root Gap Tolerances
Racking systems are welded structures. The root gap between the upright and the beam connector determines weld penetration, and therefore the load rating of the rack. Conventional plasma cutting produces a square edge with a ±0.5 mm tolerance, forcing welders to compensate with wider gaps and more filler wire. This is where yield and structural integrity intersect.
Fiber laser tube cutting enables controlled beveling—typically 30° to 45°—on the tube end. The bevel geometry must be matched to the wall thickness. For 4 mm S355JR, a 37.5° bevel with a 1.5 mm root face produces a root gap of 1.0–1.5 mm, which is optimal for GMAW penetration. For SUS304 at 3 mm wall, the bevel angle increases to 45° with a 1.0 mm root face to compensate for the alloy’s higher thermal conductivity and faster heat dissipation.
The laser’s ability to cut bevels in a single pass—without secondary machining—eliminates the 0.3–0.5 mm material loss associated with mechanical beveling. On a 6-meter tube with 12 beveled ends, this recovers 3.6–6.0 mm of stock per tube. More importantly, the ±0.05 mm tolerance on the bevel angle ensures consistent root gaps, reducing weld rework from 8% to under 2%.
Gas Delivery and Pressure Metrics
Nitrogen assist gas at 1.2–1.5 MPa is standard for S355JR and SUS304. For Al6061, oxygen at 0.8–1.0 MPa is preferred to promote exothermic reaction and increase cut speed, though this introduces a slight oxide layer that must be removed for weld-critical joints. The gas nozzle diameter—typically 1.2 mm for thin-wall, 2.0 mm for 6 mm+ wall—directly affects kerf width and dross formation. A 1.2 mm nozzle at 1.4 MPa on 3 mm S355JR produces a clean, dross-free cut at 12 m/min. Dropping to 1.0 MPa causes dross adhesion and forces a 15% speed reduction to maintain quality—a direct yield penalty.
Integrating Yield into the Production Workflow
Maximizing yield is not a single parameter; it is a system. The operator must balance kerf width, nest gap, chuck pressure, gas pressure, and bevel geometry against the alloy and wall thickness. A 2% yield improvement on a 500-ton monthly racking order saves 10 tons of steel—at S355JR pricing, that is a direct margin recovery of $8,000–$12,000 per month. The fiber laser tube system, when tuned correctly, delivers this without compromising the structural tolerances that racking systems demand.
Frequently Asked Questions
What is the optimal laser power for cutting 3 mm S355JR racking tube without sacrificing yield?
A 3–4 kW single-mode fiber laser with a 50 µm delivery fiber is optimal. It maintains a kerf of 0.15–0.25 mm and cuts at 10–14 m/min with 1.2–1.5 MPa nitrogen assist gas. Higher power increases speed marginally but widens the kerf and HAZ, reducing yield.
How does beveling with a fiber laser improve root gap tolerances compared to plasma cutting?
Fiber laser beveling holds ±0.05 mm tolerance on the bevel angle, versus ±0.5 mm for plasma. This consistency produces a root gap of 1.0–1.5 mm for 4 mm S355JR, reducing weld rework from 8% to under 2% and eliminating secondary machining losses of 0.3–0.5 mm per beveled end.
What chuck pressure should be used for SUS304 and Al6061 tube to minimize end-trim waste?
For SUS304, use 0.6–0.8 MPa to prevent ovalization. For Al6061-T6, use 0.4–0.5 MPa to avoid surface marring. Correct pressure allows end-trim reduction from 150 mm to 80 mm, recovering 70 mm per tube—a 1.2% yield gain on a 6-meter length.













