Laser Cutting vs Plasma for Thick Wall Structural Steel Pipes: Automation Interfacing and MES Integration Realities
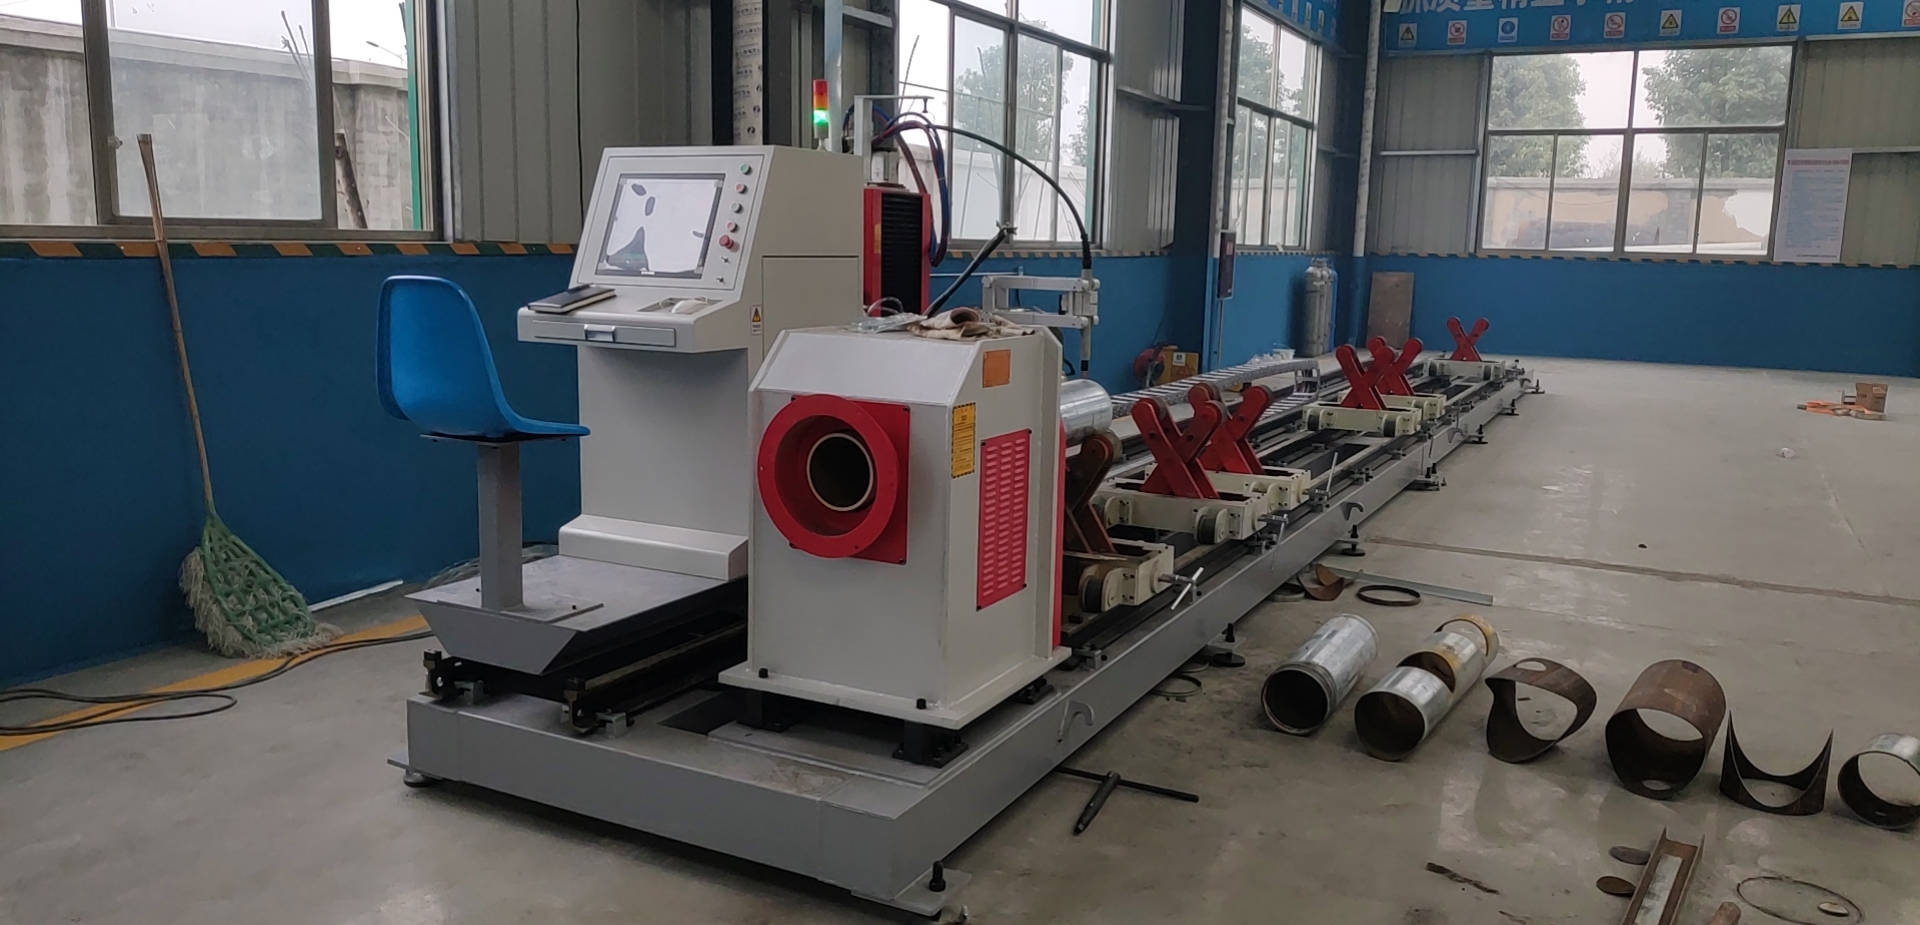
When a fabrication shop asks me to spec a tube processing cell for wall thicknesses north of 12 mm, the conversation rarely starts with the cutting head. It starts with the loader. The real decision matrix for laser cutting vs plasma for thick wall structural steel pipes is not settled at the kerf width or the heat-affected zone—it is settled at the interface between the cutting machine, the auto-bundling loader, and the MES layer that schedules the work order. A 12 kW fiber laser with a 6G chuck can out-cut a 200 A plasma torch on S355JR all day, but if the bundle loader cannot sequence 12-meter stock without manual intervention, the throughput advantage evaporates inside the first shift.
Physics and Consumables: Where the Two Processes Actually Diverge
Plasma cutting on thick-wall pipe relies on a constricted arc that transfers roughly 30–45 kW of thermal energy into the workpiece. On a 20 mm wall S355JR pipe, a 200 A oxygen plasma cut runs at 500–700 mm/min with a kerf of 3.5–4.5 mm and a HAZ extending 1.5–2.5 mm into the parent metal. The cut face carries a 3–6° bevel and dross that frequently requires secondary grinding before welding. Duty cycle on a 200 A plasma power supply sits around 60–80% at 100% rated output, which means a 12-meter pipe with 40 holes will typically force a thermal pause.
Fiber laser cutting at 12 kW on the same 20 mm S355JR uses nitrogen assist at 1.4–1.6 MPa delivered through a 1.4 mm nozzle at 25–35 bar. Cutting speed lands at 1,800–2,400 mm/min with a kerf of 0.8–1.2 mm and a HAZ under 0.3 mm. The edge is weld-ready off the table. On SUS304 at 16 mm, a 12 kW source running 100% duty cycle with nitrogen at 1.5 MPa produces a dross-free edge at 1,200–1,500 mm/min. Al6061 at 10 mm cuts cleanly at 2,000 mm/min with nitrogen, though reflectivity demands a 1.2 mm nozzle and careful pierce ramping to avoid back-reflection into the delivery fiber.
The consumable math is where plasma still wins on paper. A 200 A plasma consumable set costs roughly $45–$70 and yields 300–500 pierces on 20 mm carbon steel. A fiber laser protective window runs $30–$60 and lasts 800–1,500 hours of arc-on time, but the initial capital delta is 3–4× in favor of plasma. The break-even sits at annual throughput above roughly 4,000 tons of processed pipe—below that, plasma’s lower capex and tolerance for mill scale and rust dominate.
Upstream/Downstream Automation: The Real Bottleneck
Here is where the whitepaper-grade comparison tables usually stop, and where field engineers start sweating. A plasma cell typically feeds from a simple roller conveyor with manual bundle breakdown. A modern fiber laser tube cell integrates an auto-bundling loader with a 6-axis gantry, magnetic or vacuum end-effectors, and a bundle destacker that handles 6–12 meter stock in 3–5 ton bundles. The loader’s pneumatic chuck clamping pressure on the raw bundle runs 0.6–0.8 MPa; the cutting chuck on the machine itself runs 1.2–1.5 MPa for thin-wall and drops to 0.9 MPa on 20 mm wall to avoid ovalizing the pipe.
The MES handshake is the make-or-break layer. The loader must receive a bundle ID from the ERP, verify alloy and heat number against the work order, and signal the laser’s CNC that the correct stock is staged. On a plasma cell, this is usually a barcode scan and a manual confirmation. On a laser cell running lights-out, the MES pushes a nested cutting program keyed to the bundle’s heat number, the laser pulls the correct cutting parameter set (S355JR at 20 mm uses a different focus and gas ramp than SUS304 at 16 mm), and the auto-bundler stages the next bundle before the current one is exhausted. Any mismatch between the ERP’s alloy designation and the physical bundle triggers a hard stop—because cutting S355JR with SUS304 parameters at 12 kW will scrap the part and potentially damage the nozzle.
Comparative Technical Data: Conventional vs Fiber Laser Cell
| Parameter | Conventional Plasma / Saw | Fiber Laser Cell (12 kW) |
|---|---|---|
| Wall thickness range (S355JR) | 6–40 mm (plasma), unlimited (saw) | 1–25 mm practical, 30 mm max |
| Cut speed on 20 mm S355JR | 500–700 mm/min | 1,800–2,400 mm/min |
| Kerf width | 3.5–4.5 mm | 0.8–1.2 mm |
| HAZ depth | 1.5–2.5 mm | <0.3 mm |
| Assist gas | O2/N2 at 0.5–0.8 MPa | N2 at 1.2–1.6 MPa |
| Duty cycle at rated output | 60–80% | 95–100% |
| Loader integration | Manual or semi-auto conveyor | Auto-bundling gantry, 3–5 ton bundles |
| MES/ERP interface | Barcode scan, manual confirm | Full bidirectional, heat-number traceability |
| Edge condition post-cut | Dross, 3–6° bevel, grinding required | Weld-ready, no secondary op |
| Consumable cost per 1,000 pierces | $90–$140 | $20–$40 (windows, nozzles) |
Chuck, Gas, and Parameter Discipline on Thick Wall
Running 20 mm S355JR on a fiber laser tube cell demands parameter discipline that plasma operators never had to develop. Focus position sits at -2 to -4 mm below the surface for nitrogen cutting at 12 kW. Pierce time on 20 mm runs 1.8–2.5 seconds with a two-stage pierce: 60% power at 0.8 MPa for 1.2 s, then full power at 1.5 MPa. The chuck pneumatic pressure must hold 1.2 MPa to prevent pipe rotation during the pierce, but on thin-wall SUS304 at 2 mm, dropping to 0.7 MPa prevents deformation. The auto-bundler’s end-effector vacuum pads run at -0.6 to -0.8 bar; magnetic pads on carbon steel bundles handle 3–5 ton loads with a 1.5 safety factor.
The MES layer must push these parameters as a function of alloy and wall thickness, not as a static recipe. A 12 kW source cutting Al6061 at 10 mm needs 1.2 mm nozzle, 1.4 MPa nitrogen, and a pierce ramp that avoids back-reflection. The same source on SUS304 at 16 mm needs 1.4 mm nozzle, 1.5 MPa nitrogen, and a slower pierce. If the ERP’s alloy code does not map cleanly to the laser’s parameter library, the operator is back to manual entry—and the automation ROI collapses.
FAQ: Industrial B2B Procurement
What wall thickness limit should I spec for a fiber laser tube cell on structural pipe?
For S355JR, plan on 25 mm as the practical production ceiling with a 12 kW source and nitrogen assist at 1.5 MPa. Beyond 25 mm, plasma or saw remains more economical per meter. SUS304 and Al6061 top out lower—16 mm and 12 mm respectively—due to reflectivity and thermal management.
How does the auto-bundling loader interface with my existing MES/ERP?
Through a bidirectional OPC UA or Modbus TCP handshake. The ERP pushes bundle ID, alloy, heat number, and nested program; the loader confirms staging and the laser pulls the matching parameter set. Without heat-number traceability, you cannot run lights-out on structural steel.
What is the break-even tonnage between plasma and fiber laser for thick-wall pipe?
Roughly 4,000 tons of processed pipe per year. Below that, plasma’s lower capex and tolerance for mill scale win. Above it, the laser cell’s duty cycle, weld-ready edge, and automation integration deliver a 2–3 year payback.













