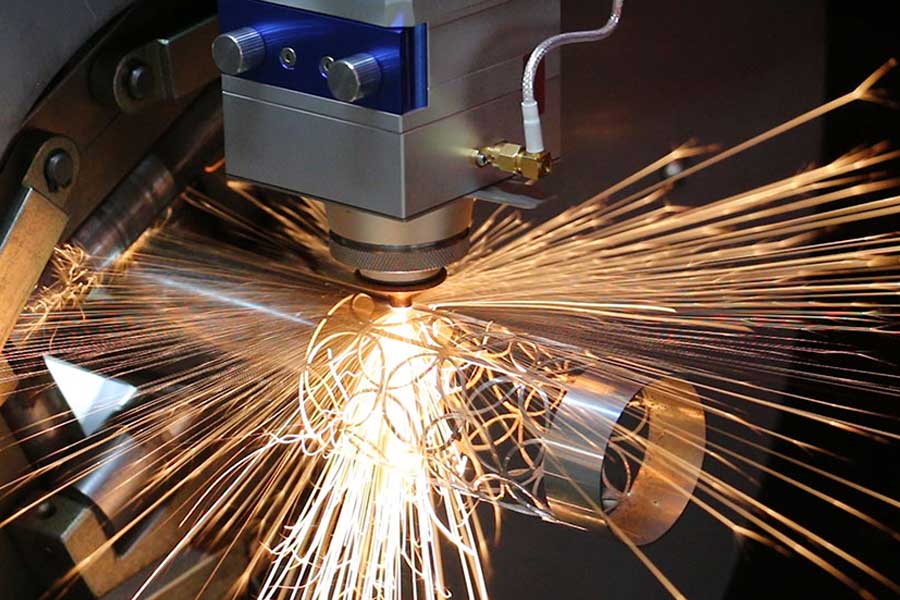
Process Metallurgy and Energy Dynamics in Orthopedic Tube Slotting
Slotting flexible orthopedic instrument tubing—typically thin-wall 304/316L stainless, nitinol, or 6061-T6 aluminum—demands a cutting regime that conventional plasma or abrasive sawing cannot economically sustain. A plasma torch running at 30–45 A on 1.5 mm SUS304 wall produces a heat-affected zone of 0.4–0.9 mm, which for a 6 mm OD cannula translates into dimensional collapse and post-process pickling. Mechanical sawing introduces burr heights of 80–150 µm and requires secondary deburring, adding labor and consumable cost. The shift toward a laser slotting machine for flexible orthopedic instruments tubing is therefore not a marketing trend but a thermodynamic and metrological necessity: fiber sources at 1070 nm couple efficiently into stainless and aluminum, delivering kerf widths of 30–80 µm with a HAZ under 50 µm when pulse parameters are tuned correctly.
Electro-Optical Conversion: Where the Real Energy Budget Lives
Wall-plug efficiency for modern single-mode and multi-mode fiber resonators sits between 30% and 42% depending on diode stack age and cooling loop stability. A 1.5 kW resonator drawing 4.2 kW from the mains at 35% conversion is dissipating roughly 2.7 kW as thermal load into the chiller circuit. On a two-shift operation (16 h/day, 300 days), that is 12,960 kWh of rejected heat annually per machine. Water-cooled chiller COP of 3.2 to 4.0 means another 3,200–4,000 kWh of compressor energy just to remove what the resonator wastes. Engineers specifying slotting cells for orthopedic tubing should track the “effective cutting efficiency”—the ratio of energy delivered to the cut zone versus total facility draw—rather than nameplate laser power. A well-tuned 1 kW source cutting 0.8 mm SUS304 at 8 m/min with 0.5 mm slot pitch achieves effective efficiency near 22%; a poorly matched 2 kW source running the same job at 40% duty cycle drops to 9%.
Pulse Frequency and Duty Cycle Trade-offs
For 316L tubing in the 0.5–1.2 mm wall range, a modulated CW regime at 1,500–3,000 Hz with 60–75% duty cycle produces clean slot walls without dross. Nitinol requires shorter pulses—200–500 Hz, 30–45% duty—to limit Ni depletion at the cut edge. Al6061-T6 slots best at 2,000–4,000 Hz with high peak power and low average power to avoid the 660°C melting pool spreading into the parent tube. These parameters directly govern gas consumption, because duty cycle determines how long the assist gas nozzle is actually doing work versus idling.
High-Pressure Assist Gas: The Hidden Operating Cost
Nitrogen assist at 1.2–1.5 MPa nozzle pressure is standard for stainless orthopedic tubing to prevent oxidation of the slot walls, which must remain passivated for autoclave cycles. A 1.5 mm nozzle orifice at 1.4 MPa consumes approximately 22–28 Nm³/h of N₂. At industrial bulk nitrogen pricing of $0.35–$0.60 per Nm³ (varies by region and contract volume), a machine running 16 h/day burns $120–$270 daily in gas alone—often exceeding the electricity bill. Oxygen assist at 0.8–1.0 MPa is cheaper per Nm³ but produces oxide dross on stainless, unacceptable for medical device slots. The optimization lever is nozzle standoff and coaxial alignment: reducing standoff from 1.2 mm to 0.6 mm can cut gas flow 25–30% while improving kerf quality, because the jet retains coherence longer.
Comparative Technical Data: Legacy vs. Fiber Laser Slotting
| Parameter | Plasma Cutting | Mechanical Sawing | Fiber Laser Slotting |
|---|---|---|---|
| Kerf width (mm) | 1.2–2.0 | 1.5–3.0 (blade thickness) | 0.03–0.08 |
| HAZ depth (µm) | 400–900 | 0 (cold cut, but work-hardened) | 20–50 |
| Burr height (µm) | 100–250 | 80–150 | <15 (with N₂ assist) |
| Energy per meter of slot (kWh) | 0.18–0.25 | 0.09–0.14 | 0.04–0.07 |
| Assist gas | Compressed air / N₂, 0.6 MPa | None (coolant only) | N₂ @ 1.2–1.5 MPa |
| Post-process deburring | Required | Required | Optional (electro-polish only) |
| Dimensional tolerance (mm) | ±0.15 | ±0.10 | ±0.02 |
| Chuck pneumatic pressure (MPa) | N/A | 0.4–0.6 (vise) | 0.5–0.7 (rotary collet) |
Chuck Dynamics and Rotary Axis Precision
Flexible orthopedic tubing—particularly cannulated reamers and guidewire sleeves—requires rotary chucking with runout under 20 µm TIR. Pneumatic collet chucks operating at 0.5–0.7 MPa provide clamping force of 400–800 N on a 6 mm OD tube, sufficient to resist torsional deflection during high-speed rotation (up to 200 rpm for slotting helical patterns). Below 0.4 MPa, tube slip becomes measurable and slot pitch drifts by 30–60 µm over a 200 mm length. Above 0.8 MPa, thin-wall 316L (0.5 mm wall) begins to ovalize. The sweet spot is narrow and must be validated per alloy and wall thickness.
Green Manufacturing Accounting
Aggregating the numbers: a fiber slotting cell replacing a plasma + deburring line for orthopedic tubing eliminates the pickling acid bath (saves 40–60 L of HNO₃/HF waste per week), removes the deburring motor load (1.1 kW continuous), and cuts total energy per finished slot by 60–70%. The trade-off is nitrogen cost, which can be mitigated by on-site PSA generation at $0.12–$0.18 per Nm³ for volumes above 40 Nm³/h. Payback on a PSA unit typically lands at 14–22 months for a two-shift orthopedic slotting operation.
Frequently Asked Procurement Questions
What wall thickness range can a fiber laser slotting machine handle on 316L orthopedic tubing?
Practical range is 0.3 mm to 3.0 mm for 316L with nitrogen assist at 1.2–1.5 MPa. Below 0.3 mm, tube distortion from clamping pressure dominates; above 3.0 mm, cutting speed drops below economic thresholds and dross adhesion increases unless oxygen assist is used, which compromises medical-grade surface finish.
How does nitrogen consumption affect total cost of ownership versus plasma?
Nitrogen at 22–28 Nm³/h and $0.35–$0.60/Nm³ adds $120–$270 per 16-hour shift. Plasma uses cheaper compressed air but incurs deburring labor, pickling chemicals, and higher scrap rates. Net TCO favors fiber laser slotting by 35–50% over a 3-year horizon when PSA nitrogen generation is installed.
What pneumatic chuck pressure is recommended for thin-wall flexible tubing?
For 0.5–1.0 mm wall 316L or nitinol, maintain 0.5–0.7 MPa at the collet. Below 0.4 MPa causes rotational slip and pitch drift; above 0.8 MPa induces ovalization on walls under 0.8 mm. Validate with a runout gauge targeting under 20 µm TIR before production release.













