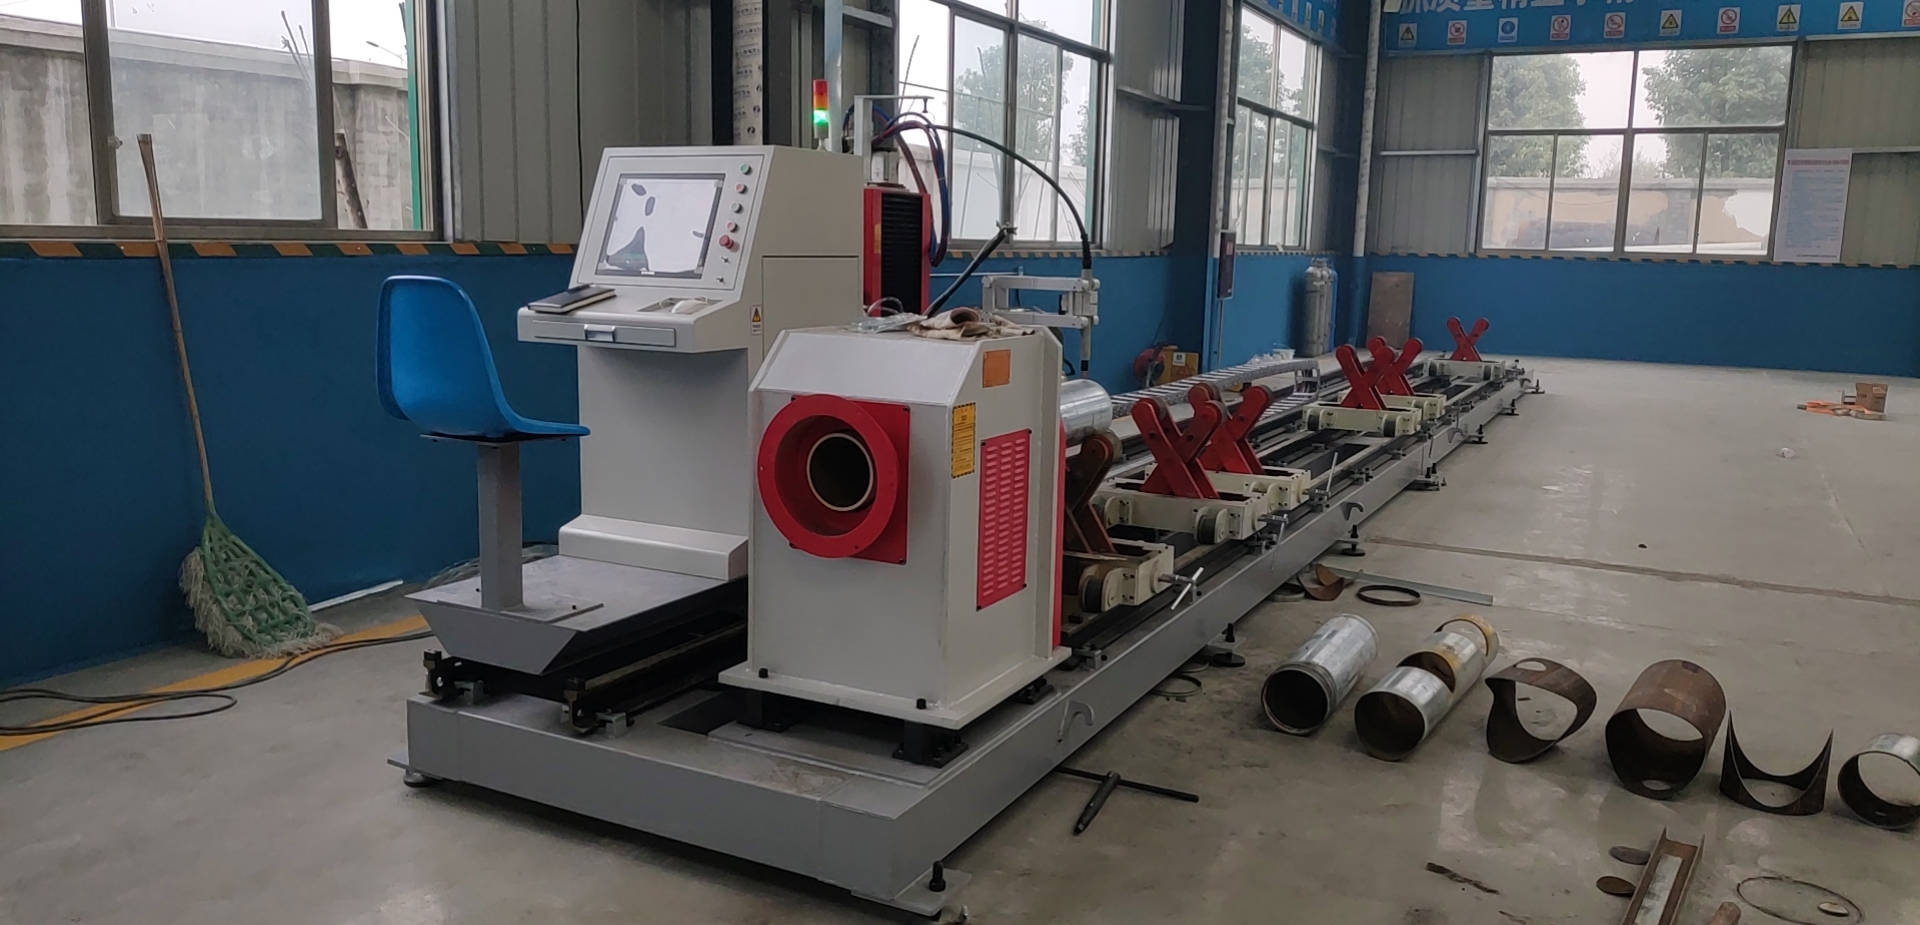
Shop-Floor Dynamics of Integrated Tube Laser Systems for Transmission Pylon Fabrication
Deploying an automated tube laser production line for power grid pylons is not a plug-and-play upgrade. It is a fundamental re-engineering of the fabrication cell, driven by the physical realities of cutting thick-walled, large-diameter structural tubing. Transmission towers—lattice sections, leg extensions, cross-arms—rely on tubular members ranging from 60 mm to 355 mm OD, with wall thicknesses spanning 3 mm to 12 mm. The dominant materials are S355JR (EN 10025-2), galvanization-grade SUS304, and occasional Al6061-T6 for specialized lightweight assemblies. Each alloy imposes distinct absorption behavior at 1070 nm, and ignoring that physics leads to dross, taper, and scrapped joints.
Material Tolerance and Laser Absorption Efficiency
Fiber laser sources operating at 1070–1080 nm deliver wall-plug efficiency of 35–40%, but coupling that beam into S355JR versus SUS304 is a different story. Mild steel S355JR exhibits absorptivity near 35–40% at room temperature, climbing to 60–70% once the melt pool forms. SUS304, with its chromium-oxide passivation layer, reflects 55–65% initially and requires a higher peak power density—typically 8–12 MW/cm²—to breach the oxide and establish a stable keyhole. Al6061 pushes this further: reflectivity above 80% at 1070 nm demands nitrogen assist at 1.4–1.6 MPa and a tighter focus spot (0.15 mm) to avoid erratic penetration.
Material tolerance is equally unforgiving. Hot-rolled S355JR tube arrives with wall-thickness variance of ±10%, ovality up to 1% of OD, and longitudinal weld seams that can sit 0.3 mm proud. A 6 kW fiber source with a 120 µm delivery fiber and a 200 mm collimator produces a kerf of 0.25–0.35 mm; if the seam rotates into the beam path without compensation, the cut edge shows intermittent notching. Rotary chuck synchronization and real-time seam detection (via capacitive or optical sensors) are non-negotiable. Chuck pneumatic pressure is typically held at 0.6–0.8 MPa for 200 mm OD tube, rising to 1.0–1.2 MPa for 355 mm OD to prevent slip during high-speed contouring at 40–60 m/min.
Comprehensive Shop-Floor Production Workflow
A functioning automated line integrates loading, cutting, and offloading into a single takt-time rhythm. The typical sequence for a pylon leg member (S355JR, 219 mm OD, 8 mm wall, 6.2 m length) runs as follows:
- Bundle loading: Chain-driven magazine feeds 12 tubes per cycle; laser profilometer scans OD and wall thickness, logging deviations to the MES.
- Chuck clamping: Front chuck at 0.8 MPa, rear chuck at 0.6 MPa; servo-driven rotation maintains ±0.05° angular accuracy.
- Cutting head positioning: 6 kW source, 1.2 MPa nitrogen for S355JR (O2 at 0.8 MPa for thicker sections above 10 mm), focal position −1.5 mm, cutting speed 3.2 m/min for 8 mm wall.
- Contour and feature cutting: Bolt holes, mitered ends, coped intersections, and weld-prep bevels executed in a single pass; no secondary drilling.
- Offloading: Servo-driven unloader transfers finished parts to a sorting table; scrap skeleton drops to a separate bin.
Cycle time for the above member averages 95–110 seconds, including pierce (1.2 s for 8 mm S355JR with nitrogen), contour, and rapid traverse. Duty cycle on the resonator is held at 60–70% to preserve diode life; the chiller maintains 22 ± 1 °C at the optics.
Comparative Technical Data: Legacy vs. Laser
| Parameter | Plasma / Mechanical Saw (Legacy) | Fiber Tube Laser (Automated Line) |
|---|---|---|
| Cut edge quality (Ra) | 12.5–25 µm (plasma), 6.3–12.5 µm (saw) | 1.6–3.2 µm |
| Heat-affected zone | 0.8–2.0 mm (plasma) | 0.05–0.15 mm |
| Dimensional tolerance | ±0.5 mm (plasma), ±0.3 mm (saw) | ±0.05 mm |
| Secondary operations | Deburring, drilling, reaming | None (single-pass features) |
| Cycle time (219 mm OD, 8 mm wall, 6.2 m) | 240–360 s (multi-step) | 95–110 s |
| Consumable cost per meter | USD 0.45–0.80 (electrodes, blades) | USD 0.12–0.22 (gas, optics amortized) |
| Material utilization | 82–88% | 94–97% (nesting + kerf control) |
| Labor per shift | 3–4 operators | 1 operator + 1 loader |
Gas Delivery and Thermal Management
Nitrogen assist for S355JR is delivered at 1.2–1.5 MPa through a 1.5 mm nozzle; oxygen for sections above 10 mm runs at 0.6–0.9 MPa to promote exothermic reaction and improve edge wetting. For SUS304, nitrogen at 1.4–1.6 MPa is mandatory to suppress oxidation and maintain a clean, weldable edge. Flow rates hover at 18–25 L/min. The pierce routine for 12 mm SUS304 uses a ramped power profile—30% duty for 0.4 s, then 100% for 1.1 s—to avoid spatter adhesion on the protective lens. Lens protection via cross-jet at 0.4 MPa extends consumable life to 400–600 hours.
Integration and Throughput Reality
Real-world throughput for a single automated cell handling pylon members averages 28–34 parts per shift, assuming 85% OEE. The bottleneck is rarely the laser; it is the loading magazine and the offload sorting logic. Shops that pair the laser with a robotic sorting arm and MES-driven nesting report OEE climbing to 90% and scrap dropping below 0.8%. The physics of absorption, the metallurgy of S355JR and SUS304, and the mechanical discipline of chuck pressure and gas delivery determine whether the line delivers 30 parts or 18.
What wall thickness can a 6 kW fiber laser cut on S355JR pylon tube?
With nitrogen assist at 1.2–1.5 MPa, a 6 kW source cleanly cuts S355JR up to 10 mm wall. Above 10 mm, oxygen assist at 0.6–0.9 MPa is recommended, extending capability to 14 mm with acceptable edge quality (Ra 3.2–6.3 µm).
How does SUS304 affect laser absorption compared to mild steel?
SUS304 reflects 55–65% of 1070 nm radiation at room temperature versus 35–40% for S355JR. This requires higher peak power density (8–12 MW/cm²) and nitrogen assist at 1.4–1.6 MPa to breach the chromium-oxide layer and stabilize the keyhole.
What chuck pneumatic pressure is required for 355 mm OD tube?
For 355 mm OD pylon tube, front chuck pressure should be set at 1.0–1.2 MPa and rear chuck at 0.8–1.0 MPa. This prevents slip during contouring at 40–60 m/min while avoiding tube deformation beyond 0.05 mm ovality.













