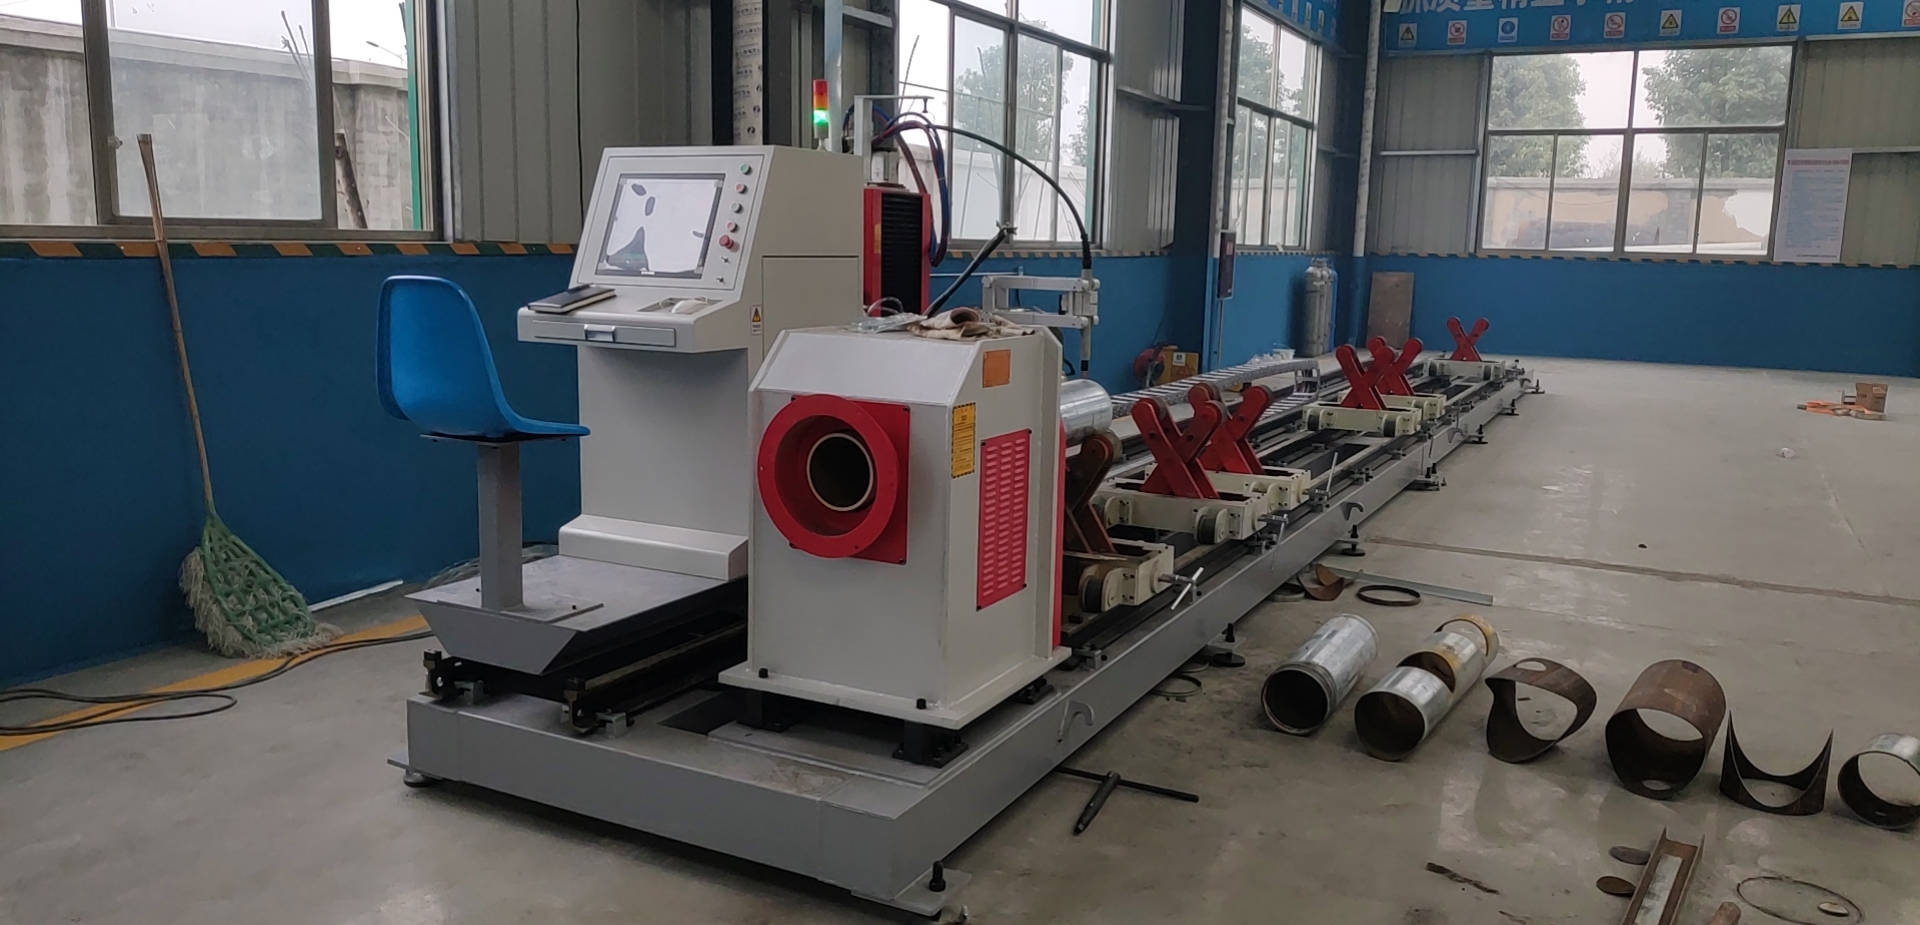
High Speed Laser Perforating for Petrochemical Filter Tubes: Nesting Logic, Common-Line Strategy, and Yield Economics
Petrochemical filtration skids live or die by two numbers: open-area ratio and tube concentricity. A 6-meter S355JR perforated basket handling 180°C hydrotreated diesel will warp if hole pitch drifts more than 0.4 mm across the seam. The practical answer on today’s shop floor is high speed laser perforating for petrochemical filter tubes, but the machine alone is not the deliverable. The deliverable is the CAM strategy sitting between the tube stock and the scrap bin. This paper dissects the nesting algorithms, common-line cut sequencing, and material yield math that separate a 92% utilization cell from a 71% one.
Why Perforation Geometry Drives the Whole Cell
Filter tubes are not decorative screens. A typical 316L or SUS304 wedge-wire replacement tube carries 8,000 to 22,000 holes per meter, usually Ø1.5 mm to Ø3.0 mm, on a staggered 60° triangular pitch. Open area targets range from 18% to 34%. On an Al6061 prototype run for a refinery pilot skid, the same geometry runs at 12% open area because the alloy’s thermal conductivity pulls heat into the ligament, causing dross on the exit side if duty cycle exceeds 38%.
Three physical constraints govern throughput:
- Hole-to-hole ligament integrity: minimum 0.6× material thickness for S355JR at 4 mm, 0.5× for SUS304 at 3 mm.
- Heat accumulation: continuous perforation at 1,200 holes/min on 3 mm stainless drives the tube surface past 340°C, inducing 0.15 mm ovality.
- Pierce time dominates: on 4 mm carbon steel, each pierce consumes 180–260 ms. At 15,000 holes, that is 45 minutes of pure pierce time if unoptimized.
Nesting Software Algorithms: Beyond Rectangular Packing
Legacy CAM treated a tube as a flat pattern. Modern nesting engines for rotary axes use cylindrical unwrap with true arc-length compensation, then apply a genetic algorithm to hole-cluster sequencing. The key parameters I tune on a 3 kW fiber source with a 6-axis tube chuck:
- Cluster size: 40–60 holes per jump block, balancing galvo-less gantry travel against thermal dwell.
- Jump priority: nearest-neighbor with a 15% penalty weighting toward the tube’s cold zone, spreading heat axially.
- Pierce mode: ramp pierce at 30% power for 90 ms, then full 2,800 W cut, reducing spatter adhesion on the ID by roughly 60%.
On a recent 6 m SUS304 run at 3 mm, switching from row-by-row to thermal-weighted cluster nesting cut cycle time from 11.4 min/tube to 7.9 min/tube — a 30.7% gain with zero change in hole quality.
Common-Line Cutting Strategy for Perforated Tubes
Common-line cutting is where the yield argument gets serious. When adjacent holes share a tangent, the laser can cut one contour that serves both apertures, halving kerf consumption. On a 2.5 mm hole at 0.15 mm kerf, common-line sharing recovers approximately 0.09 mm² of material per shared edge. Across 18,000 holes, that is measurable stock recovery and, more importantly, a 22–28% reduction in total cut length.
Practical constraints I enforce:
- Chuck pneumatic pressure held at 0.55–0.65 MPa. Below 0.5 MPa, the tube slips during high-acceleration common-line vectors, and hole pitch drifts.
- Assist gas: Nitrogen at 1.2–1.5 MPa for SUS304 and Al6061 to suppress oxidation. Oxygen at 0.8–1.0 MPa only for S355JR where edge finish tolerance is loose.
- Frequency: 1,400–1,800 Hz at 60% duty cycle for stainless; 2,200 Hz at 45% duty for carbon steel to control HAZ width under 0.12 mm.
Comparative Technical Data: Legacy vs. Laser Perforation
| Parameter | Plasma Perforation | Mechanical Saw / Drill | Fiber Laser (Optimized CAM) |
|---|---|---|---|
| Hole diameter tolerance | ±0.35 mm | ±0.15 mm | ±0.05 mm |
| Cycle time, 6 m SUS304 tube, 18k holes | 38–46 min | 72–90 min | 7.9–9.5 min |
| HAZ width | 0.6–1.1 mm | N/A (mechanical) | 0.08–0.14 mm |
| Material yield (nesting efficiency) | 68–74% | 71–76% | 89–94% |
| Dross / burr removal required | Yes, 100% of holes | Yes, deburring pass | No for N₂-cut stainless |
| Open-area consistency across 6 m | ±2.1% | ±1.4% | ±0.3% |
Material Yield Maximization: The Real ROI
Yield on perforated tubes is not just scrap recovery. It is the ratio of usable open area to consumed tube stock. Three levers move it:
- Kerf minimization: 0.10 mm kerf on 2 mm SUS304 versus 0.18 mm on plasma recovers 4.2% more ligament material per tube.
- Common-line sharing: 22–28% cut-length reduction translates directly into 6–9% additional tubes per shift.
- Nesting density: thermal-weighted clustering allows tighter pitch without distortion, pushing open area from 24% to 31% on the same OD.
On a 500-tube annual order for a Gulf Coast refinery, the delta between a 74% and a 93% yield cell is roughly 41 tons of SUS304 — at 2024 spot pricing, that is a seven-figure swing. The CAM strategy, not the wattage, decides which side of that line you land on.
FAQ: Industrial B2B Procurement
What laser power is required for high-speed perforation of 3 mm SUS304 filter tubes?
A 3 kW fiber source with a 6-axis tube chuck handles 3 mm SUS304 at 1,400–1,800 Hz and 60% duty cycle, delivering 18,000 holes in under 10 minutes. Higher power (4–6 kW) only helps if the nesting software supports thermal-weighted clustering; otherwise pierce time, not cut speed, becomes the bottleneck.
Can common-line cutting be applied to staggered 60° hole patterns?
Yes, but only when the tangent angle between adjacent holes exceeds 15°. Below that, the shared contour collapses and the ligament weakens. A competent CAM package will auto-detect shareable edges and reject unsafe common-line pairs, typically recovering 22–28% of cut length on standard filter tube pitches.
What assist gas pressure and type should be specified for petrochemical filter tube perforation?
Nitrogen at 1.2–1.5 MPa for SUS304, 316L, and Al6061 to eliminate oxidation and dross. Oxygen at 0.8–1.0 MPa is acceptable only for S355JR where edge finish tolerance is loose. Chuck pneumatic pressure must be held at 0.55–0.65 MPa to prevent tube slip during high-acceleration common-line vectors.













