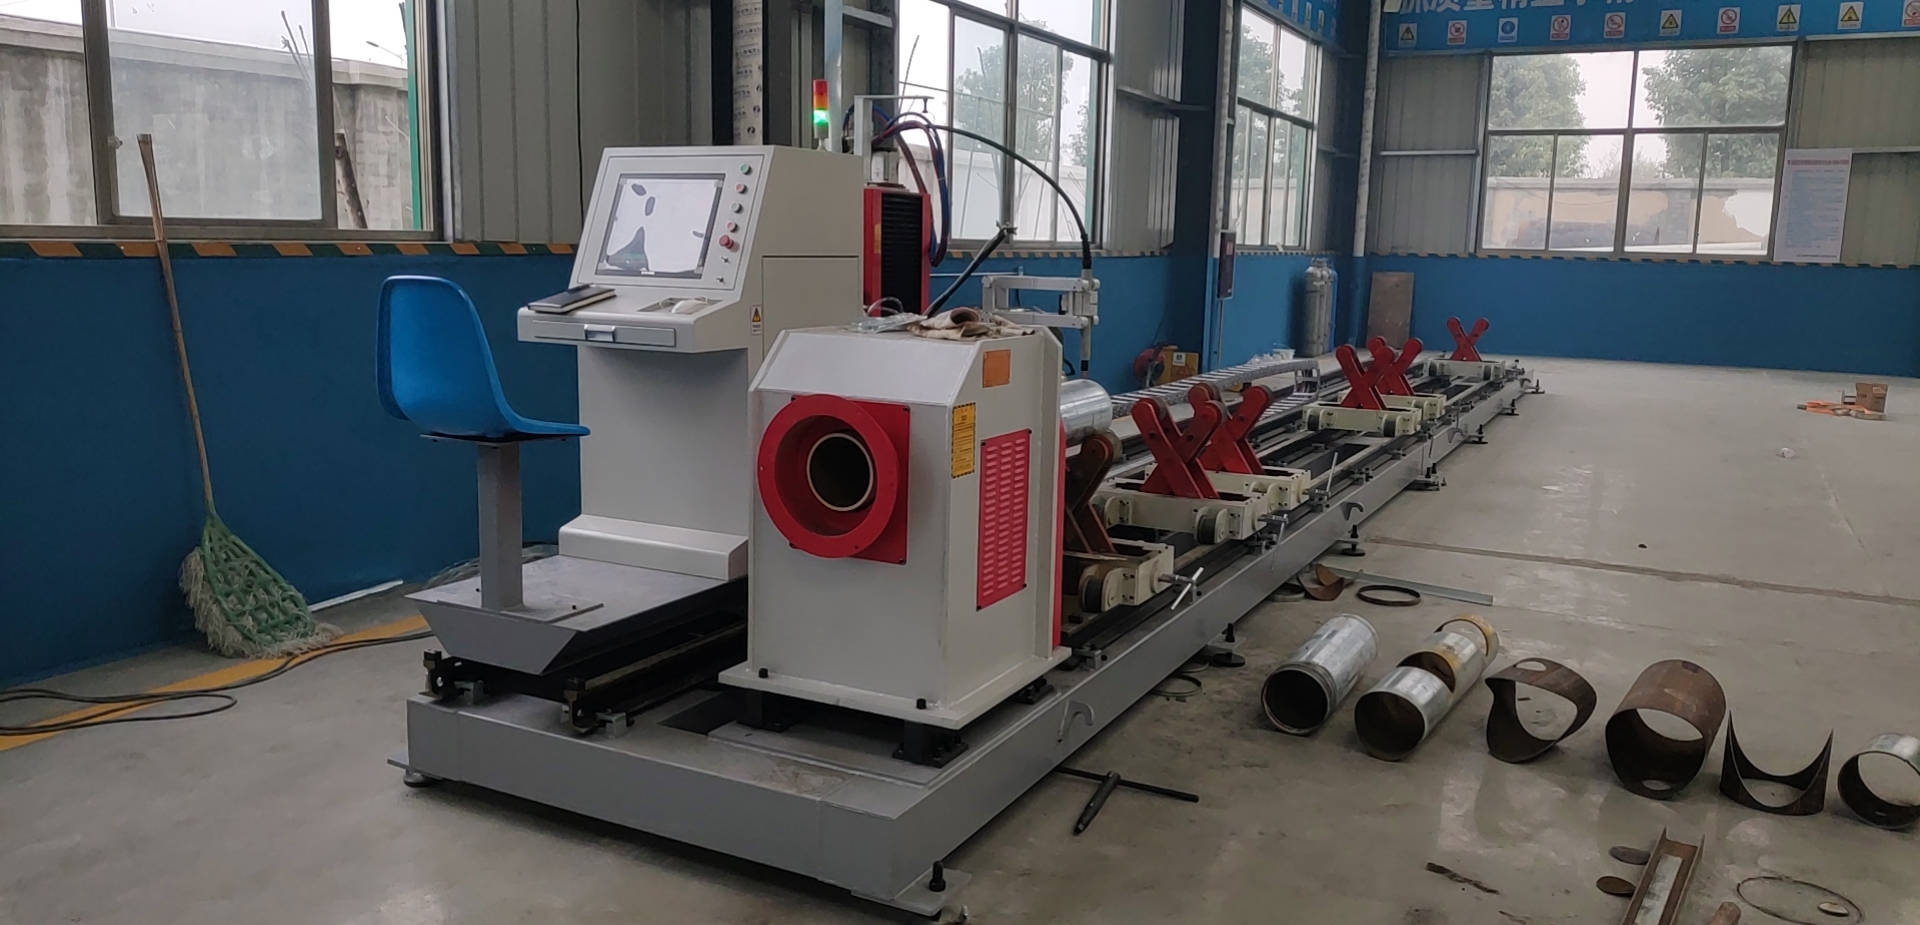
Process Metallurgy and Throughput Physics in Military Vehicle Cage Fabrication
Military vehicle anti-roll cages, blast-attenuation frames, and roof-mounted weapon station hoops are not consumer roll bars. They are certified structural weldments typically specified to AEP-55 / STANAG 4569 blast criteria, fabricated from seamless or DOM tube in grades such as S355JR, 4130 chromoly, SUS304 austenitic stainless, and Al6061-T6 for weight-sensitive appliqué subframes. Wall thickness ranges from 3.0 mm to 8.0 mm, tube OD from 38 mm to 89 mm. The fabrication bottleneck is never the laser source itself — it is the synchronization between the cutting head, the bundle loader, and the MES work order. This paper examines the automation architecture required to hold ±0.15 mm cut consistency across a 24/7 defense production cell, and why high consistency pipe laser cutting for military vehicle cage demands treating the loader and the ERP layer as first-class machine components rather than peripheral accessories.
Why Legacy Cutting Methods Fail the Consistency Envelope
Plasma and mechanical sawing remain in service on older defense lines, but their process capability collapses when applied to thin-wall 4130 or Al6061 cage nodes. Plasma introduces a heat-affected zone of 0.8–2.5 mm with dross adhesion on the ID, requiring secondary reaming that destroys the tube’s concentricity. Abrasive sawing produces burrs up to 0.4 mm and cannot generate the saddle-notch geometry required for coped joints without a separate milling operation. The laser cell eliminates both by delivering a focused 1.07 µm beam at 4–6 kW with a kerf of 0.15–0.25 mm and a recast layer under 20 µm.
| Parameter | Plasma Cutting | Mechanical Sawing | Fiber Laser Cell (Automated) |
|---|---|---|---|
| Cut tolerance (OD/ID) | ±0.8 mm | ±0.5 mm | ±0.15 mm |
| HAZ width | 0.8–2.5 mm | None (mechanical) | <0.05 mm |
| Dross / burr | Heavy ID dross | 0.2–0.4 mm burr | Negligible, N2-assisted |
| Cycle time per node | 45–70 s | 30–55 s | 8–14 s |
| Assist gas | Air/O2, 0.6 MPa | None | N2 1.2–1.5 MPa (SUS/AL), O2 0.8 MPa (S355JR) |
| Automation interface | Manual load | Manual load | Auto-bundling loader + MES handshake |
| First-pass yield (cage node) | 82–88% | 85–90% | 98.5–99.4% |
Upstream Interfacing: Auto-Bundling Loader Kinematics
The upstream loader is where consistency is won or lost. A six-meter bundle of 60 mm OD S355JR tube weighs 340–420 kg. The loader must index individual tubes into the chuck axis without inducing ovality. Pneumatic chuck clamping pressure is held at 0.6–0.8 MPa for thin-wall SUS304 (3 mm) and raised to 1.0–1.2 MPa for 8 mm 4130. Exceeding 1.4 MPa on 3 mm Al6061-T6 causes measurable wall deformation at the jaw contact patch — a defect that only surfaces at the blast-test stage.
Bundle-to-single-tube separation uses a magnetic or pneumatic destacker with a 12–18 mm lift stroke, feeding a V-groove roller bed with servo-driven axial positioning accurate to ±0.05 mm. The loader PLC must publish tube ID, heat lot, and length to the cutting cell via Profinet or EtherCAT at a 4 ms cycle. If the loader and laser controller are not on a shared clock, the chuck will begin rotation before the tube is fully seated, producing a 0.3–0.5 mm axial drift across a 200-piece batch — enough to scrap an entire cage weldment set.
Downstream Automation and the MES/ERP Handshake
Post-cut, the cell must discharge finished nodes into a buffered chute or a second auto-bundling stacker without operator contact. The critical integration point is the MES work order. Each cage assembly carries a serialized traveler. The laser cell queries the MES for the next work order, pulls the CAD/CAM nesting program, verifies the tube heat lot against the material certificate in the ERP, and only then releases the loader. Cutting parameters are pushed per-material: SUS304 runs at 4.5 kW, 2000 mm/min, N2 at 1.4 MPa; S355JR at 5.0 kW, 2600 mm/min, O2 at 0.8 MPa; Al6061-T6 at 3.5 kW, 3200 mm/min, N2 at 1.5 MPa.
Duty cycle on the fiber source is held at 60–70% during continuous cage production to preserve beam quality and diode life. The MES logs every cut with timestamp, gas pressure, and chuck pressure, creating a traceable record for defense audits. Without this ERP-level integration, a cage batch cannot be certified — the paper trail is as important as the cut itself.
Failure Modes and Mitigation
- Chuck pressure drift on thin-wall Al6061: install closed-loop pressure transducers with 0.02 MPa resolution.
- Loader-to-chuck clock desync: enforce PTP (Precision Time Protocol) across the cell network.
- MES work order mismatch: barcode verification at the loader throat before tube release.
- Nitrogen pressure sag at 1.5 MPa during peak draw: buffer tank sized to 2× cell consumption.
FAQ: Procurement and Integration Questions
What loader-to-laser synchronization latency is acceptable for military cage production?
Sub-10 ms end-to-end is the practical target. Anything above 15 ms introduces axial drift that exceeds the ±0.15 mm tolerance on coped nodes, particularly on 3 mm wall SUS304.
Can the MES/ERP layer run on the same network as the laser controller?
Yes, but it must be segmented with a managed switch and PTP-enabled. Mixing office ERP traffic with the real-time cell network without VLAN isolation causes jitter that corrupts the work-order handshake.
What gas delivery pressure is required for a mixed-material cage cell?
Size for 1.5 MPa nitrogen and 0.8 MPa oxygen at the nozzle, with a buffer tank rated to 2.0 MPa. Peak draw during simultaneous cutting and purge cycles will sag a marginal supply below the threshold for clean Al6061 cuts.













